Our Plush Toy Factory — Built for Reliable Plush Production at Scale
Give your plush program the manufacturing capacity, process control and production visibility needed for dependable execution. Ewin Toys connects core processes under one integrated factory system, helping brands manage complex SKUs, large-volume orders and repeat production with fewer handoff risks.
95,000+ m² Manufacturing System | 1,900+ Workforce | 1,200+ Sewing Team | 100+ Quality Personnel | 150+ Packaging Team | Cutting / Embroidery / Sewing / Stuffing / Assembly / QC / Packing
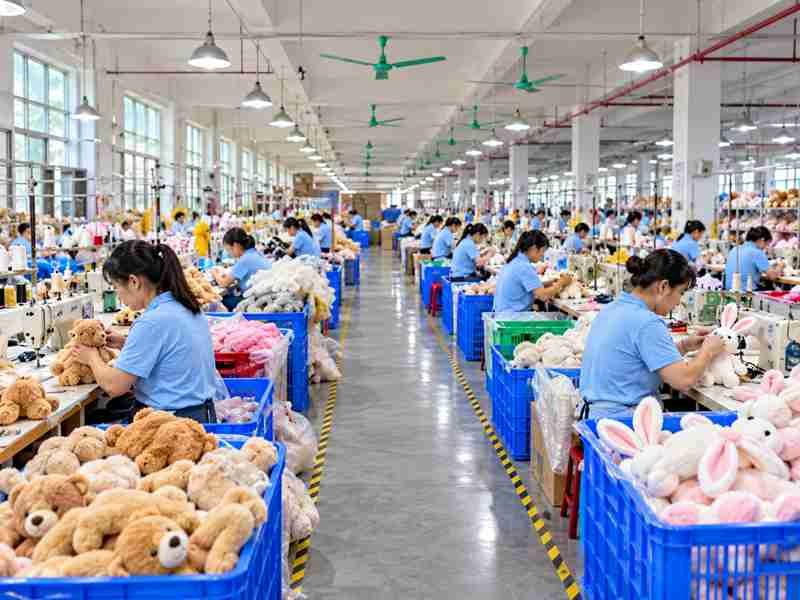
Ewin Toys Factory at a Glance
Factory scale matters when it gives development, production, quality, and delivery teams enough resources to execute complex custom programs.
95,000+ m2 System
1,900+ Workforce
60+ Development Center
Approx. 2,490 Workstations
Development-to-Bulk Control
Product-to-Delivery System
Plush Product Types Manufactured Across the Factory
Different plush formats use different materials, workstations, inspection points, assembly methods, and production controls inside the Ewin manufacturing system.
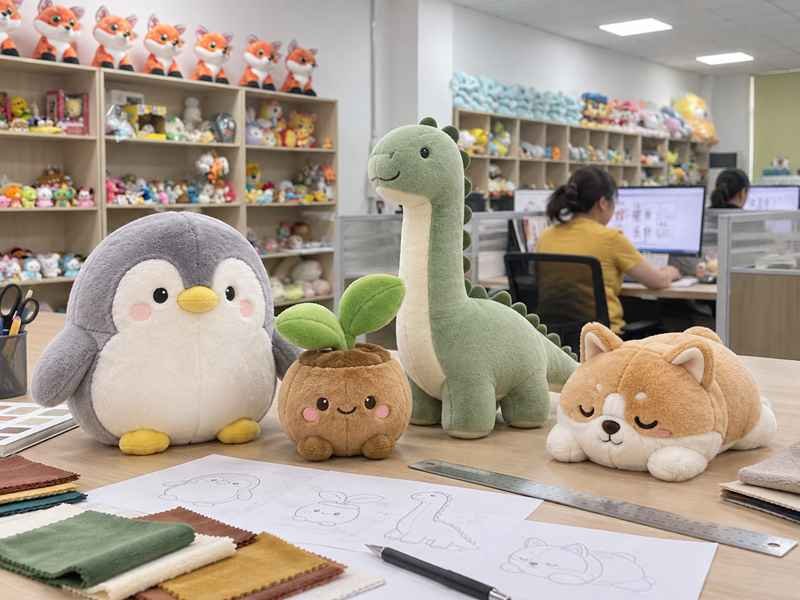
Custom Plush Toys
- Manufacturing focus: repeatable shape and construction.
- Typical use: retail, gifting, IP, DTC, and merchandise programs.
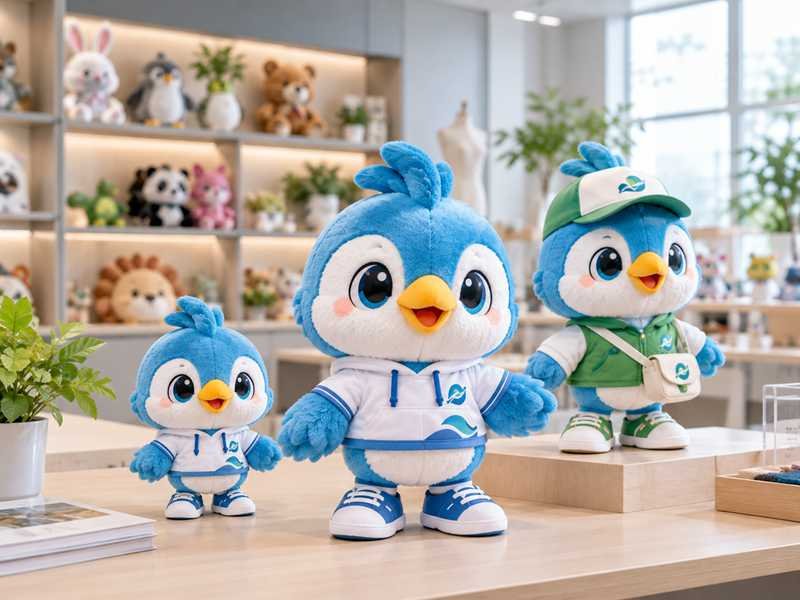
Character & Mascot Plush
- Manufacturing focus: character fidelity at scale.
- Typical use: brands, teams, venues, entertainment, and licensed programs.
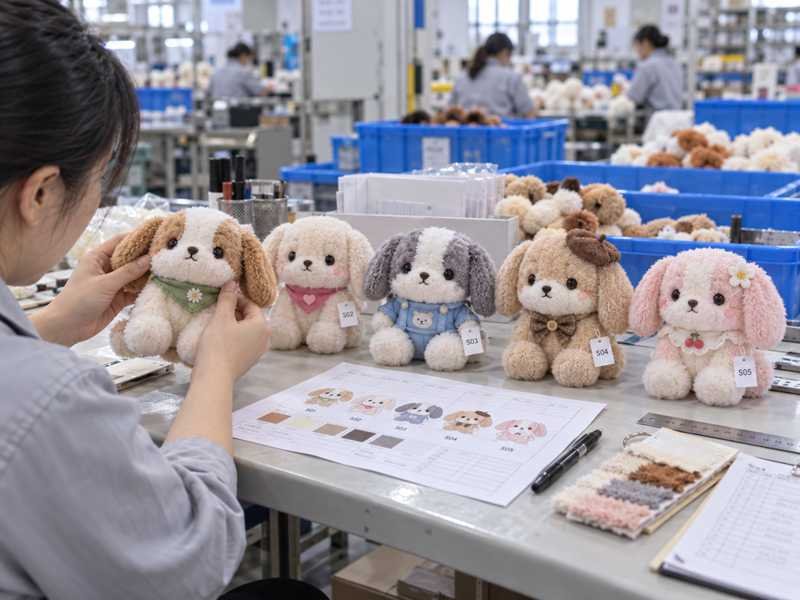
Collectible Plush
- Manufacturing focus: detail, finish, and series language.
- Typical use: designer, limited-edition, and collectible programs.
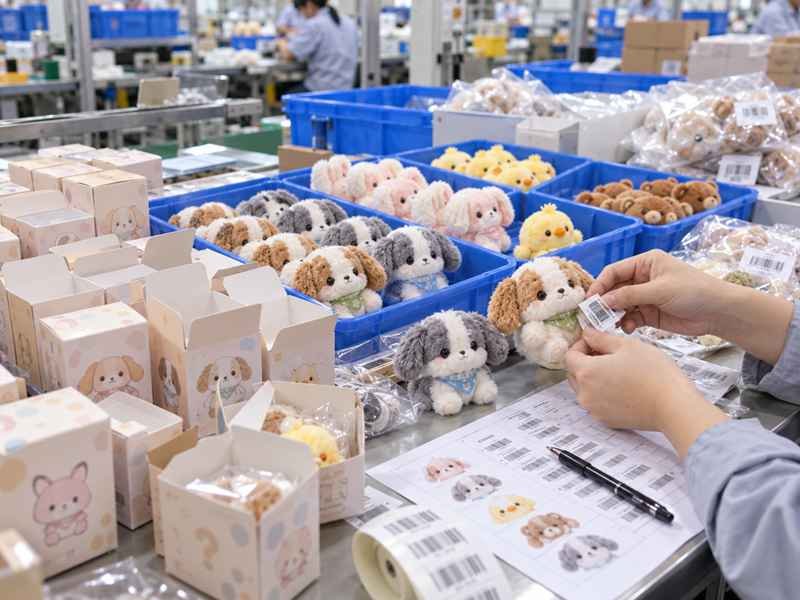
Mini & Blind Box Plush
- Manufacturing focus: small-detail repeatability and SKU control.
- Typical use: mini collections, blind boxes, and collectible drops.
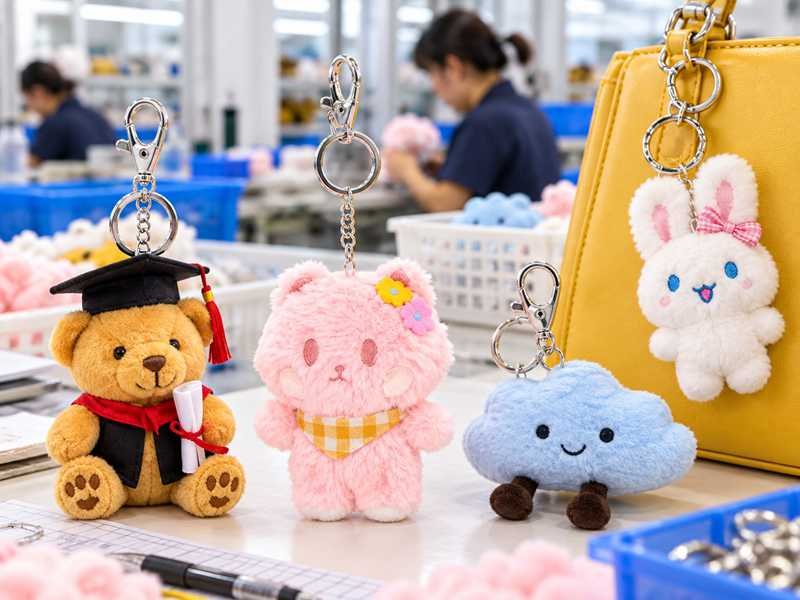
Keychains & Bag Charms
- Manufacturing focus: small-part sewing and hardware attachment.
- Typical use: fashion, IP, gift, and accessory programs.
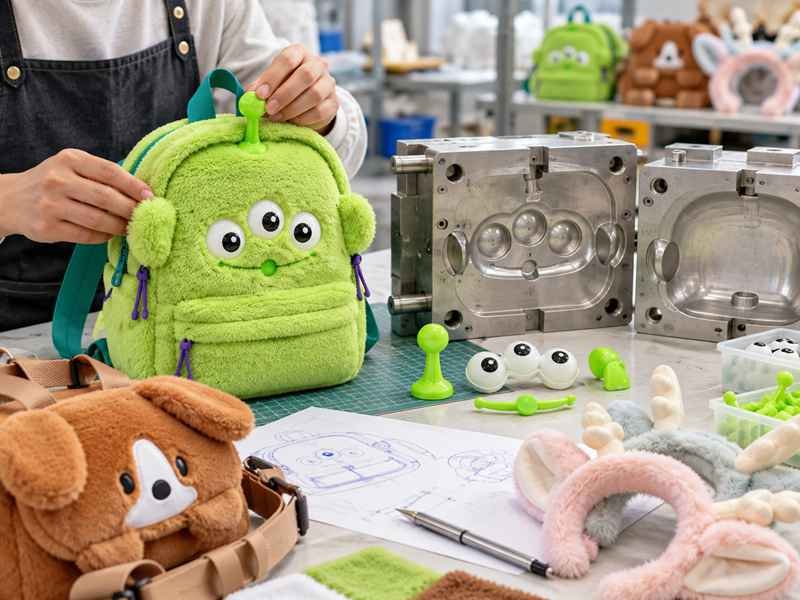
Plush + Hard Components
- Manufacturing focus: repeatable soft-hard integration.
- Typical use: stylized collectibles, characters, and functional products.
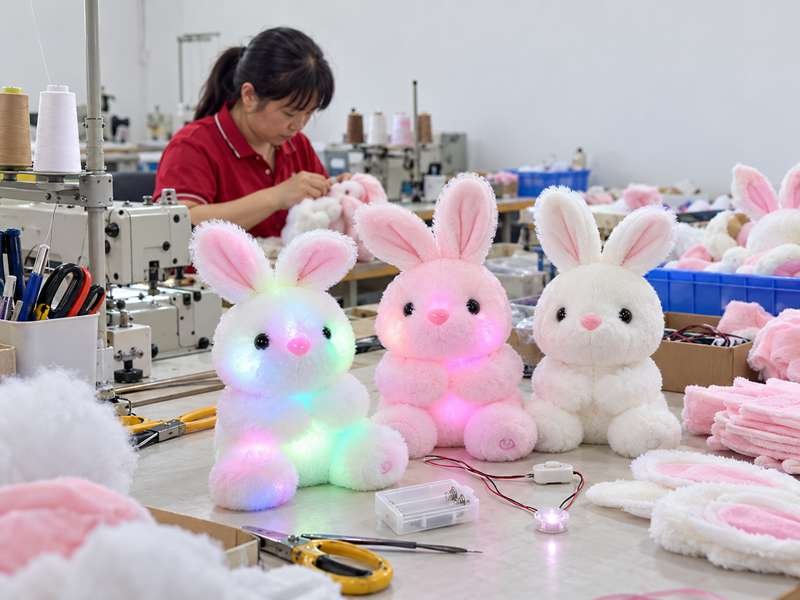
Electronic & AI Plush
- Manufacturing focus: soft-goods and module integration.
- Typical use: sound, light, interactive, and AI-enabled plush.
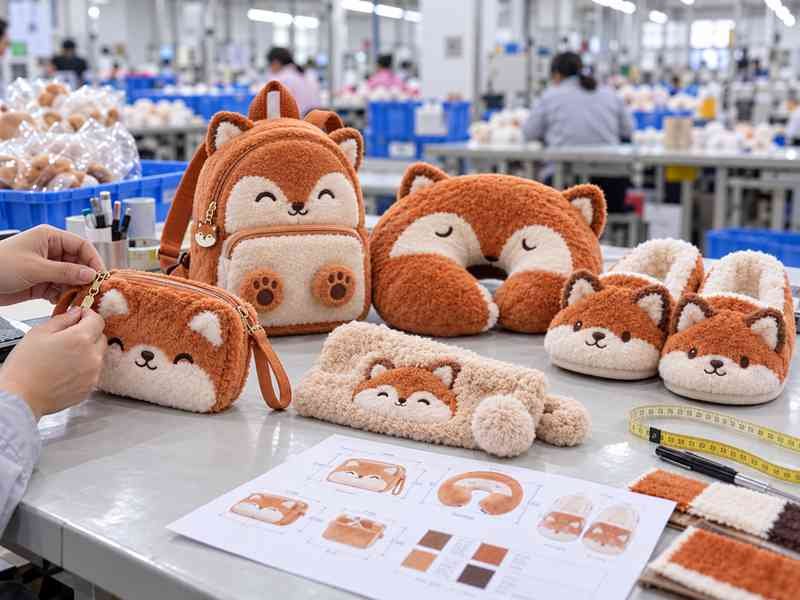
Lifestyle Plush Merchandise
- Manufacturing focus: character styling plus functional construction.
- Typical use: lifestyle, retail, IP, and merchandise collections.
Factory Support for Different Commercial Programs
The same manufacturing floor must solve different problems depending on who approves the product, how it is sold, and when it must launch.
Global Brand Teams
- Factory priority: consistency, scale, and controlled change.
- Useful inputs: brand standards, forecasts, approved references.
IP Owners
- Factory priority: fidelity and confidentiality.
- Useful inputs: character guides, approval comments, launch plan.
Licensing Companies
- Factory priority: approval traceability and version control.
- Useful inputs: approval route, legal copy, market scope.
Toy Companies
- Factory priority: product fit and scalable manufacturing.
- Useful inputs: SKU list, target market, release schedule.
Collectible Brands
- Factory priority: finish quality and series language.
- Useful inputs: collection plan, packaging concept, drop date.
Retail & Private Label
- Factory priority: retail readiness and delivery discipline.
- Useful inputs: retailer guide, packaging brief, set date.
Merchandise Agencies
- Factory priority: clear handover and timeline control.
- Useful inputs: campaign brief, quantity, deadline, artwork.
Technology & AI Teams
- Factory priority: interface control and assembly consistency.
- Useful inputs: module envelope, hardware sample, revision list.
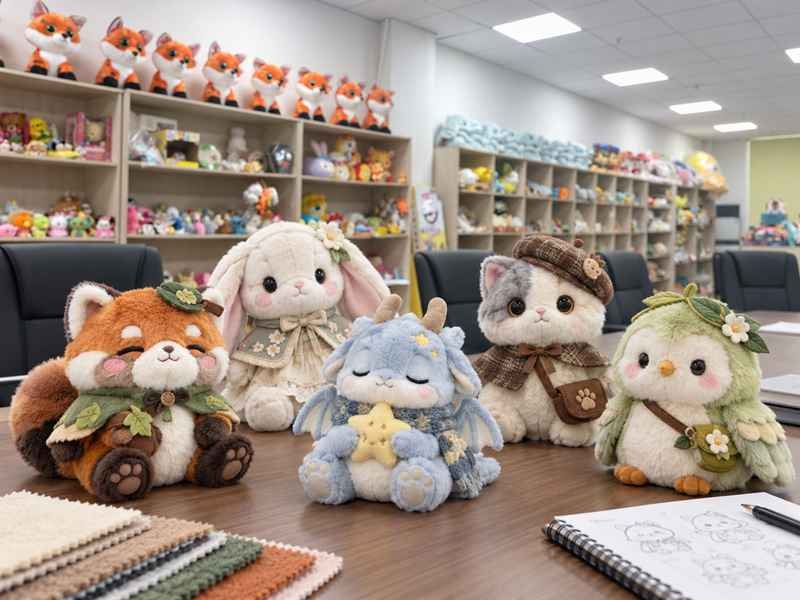
Manufacturing Zones Connected Through One Factory Route
Each area has a defined handoff, helping approved materials and product information move through production without losing identity or version control.
Development Center
Material Warehouse
Cutting Area
Embroidery & Printing
Sewing Area
Stuffing & Shaping
Hand Assembly
QC & Testing
Packaging & Warehouse
Plush Fabrics Selected for Product and Production Fit
Fabric choice is controlled by appearance, pile, handfeel, decoration, sewing behavior, availability, and the approved sample – not by material name alone.
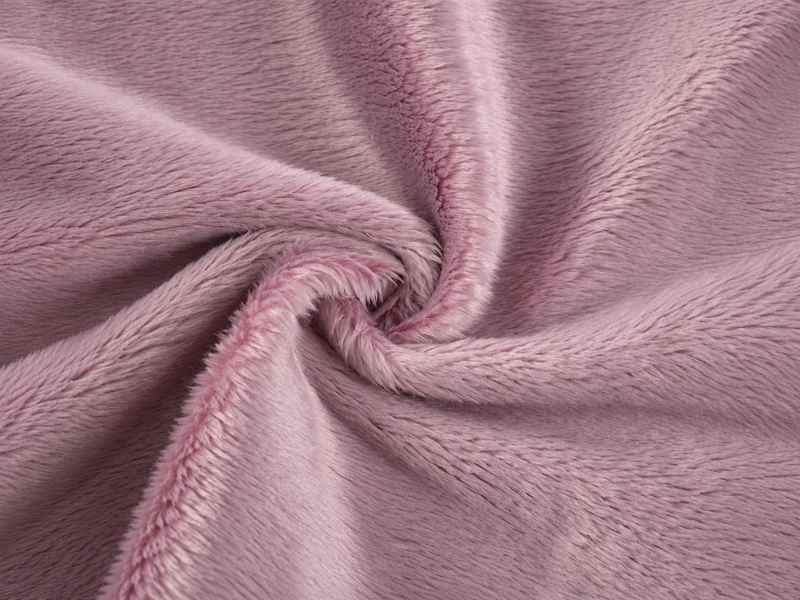
Super Soft Short Pile
- Control: GSM, pile height, color, nap, approved swatch.
- Watch: supplier-to-supplier differences under the same material name.
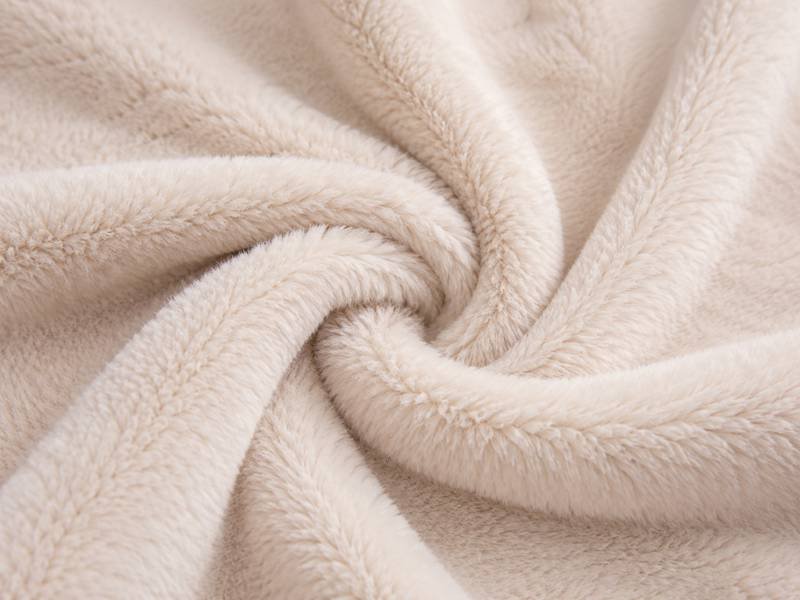
Medium Pile Plush
- Control: density, pile direction, cutting, grooming.
- Watch: decoration visibility and bulk color consistency.
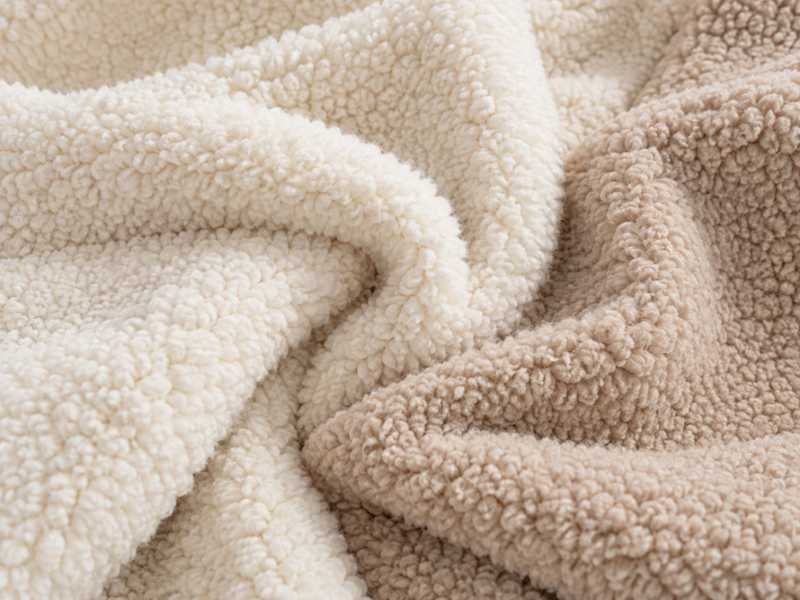
Sherpa & Teddy Textures
- Control: curl, thickness, color, seam allowance.
- Watch: small facial details becoming visually buried.
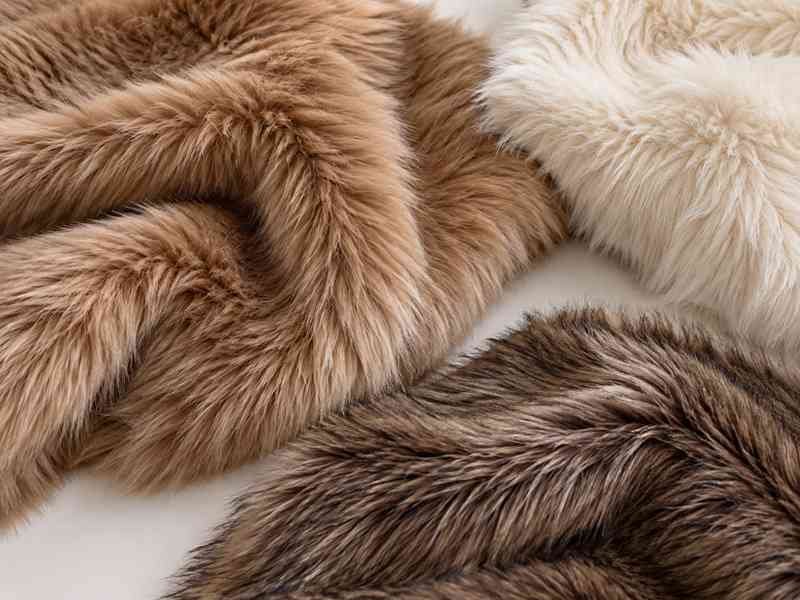
Faux Fur & Long Pile
- Control: pile length, direction, grooming, approved finish.
- Watch: face details disappearing under the fur.
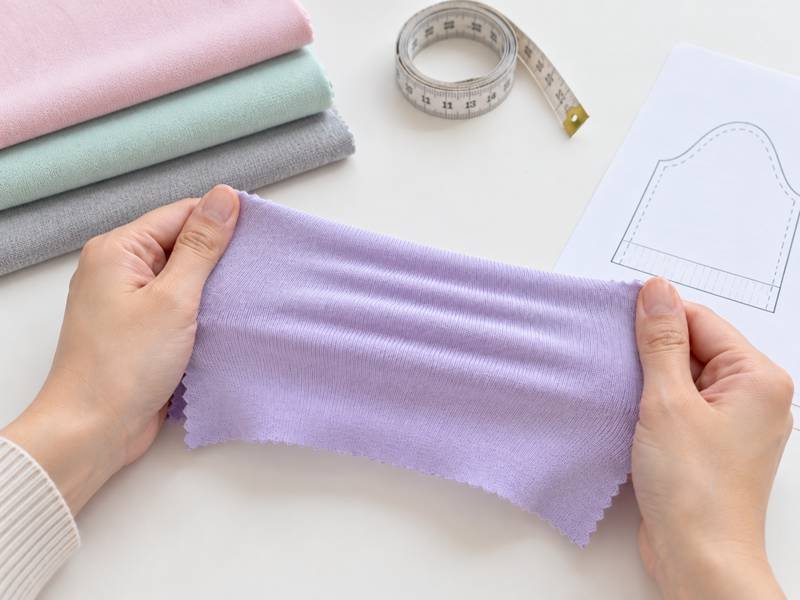
Flat & Structural Fabrics
- Control: thickness, stretch, backing, print compatibility.
- Watch: mixing materials with different stretch or shrink behavior.
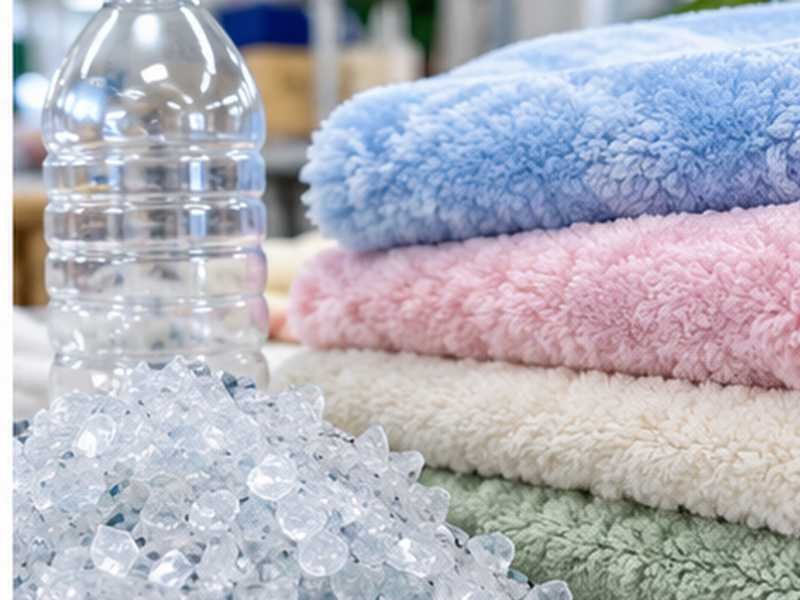
Recycled Material Routes
- Control: source, specification, batch, claim scope.
- Watch: using a sustainability claim without matching evidence.
Trims and Supporting Materials Are Production Specifications
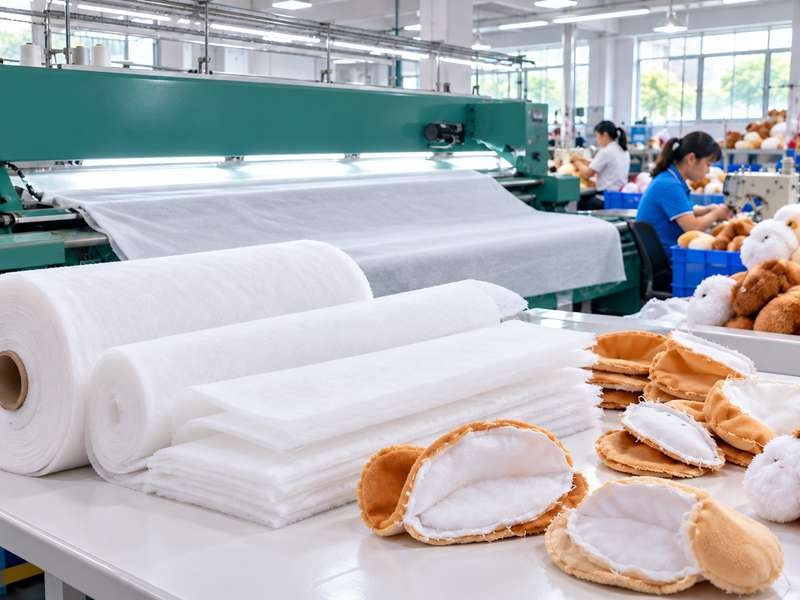
Linings & Interlinings
Lining and interlining materials support bags, clothing, cavities, internal reinforcement, or shape control. Thickness, GSM, stretch, stiffness, location, and function need to be defined so a later substitution does not change fit, handfeel, or assembly.
- Record material and thickness.
- Link each lining to its use location.

Sewing Threads
- Control size, color, and use location.
- Separate structural thread from visible decorative requirements.
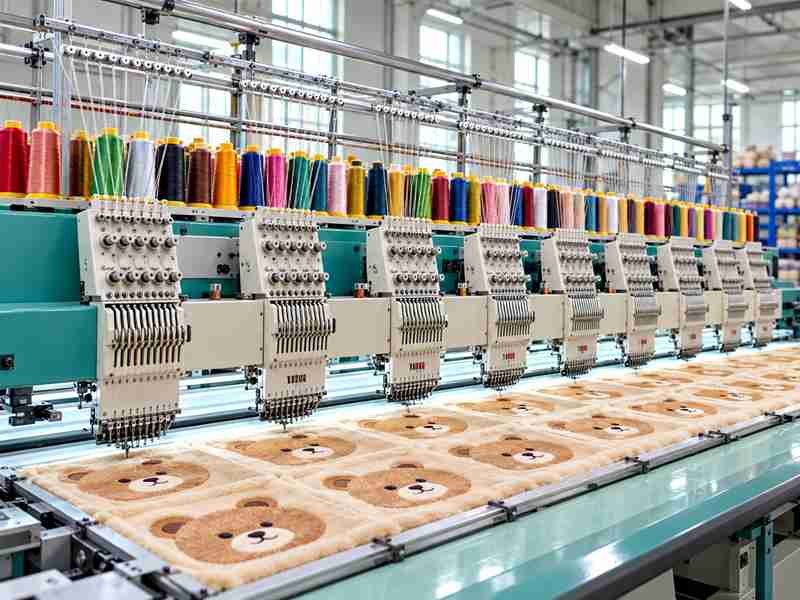
Embroidery Threads
- Lock thread color and program version.
- Keep face embroidery tied to approved coordinates.
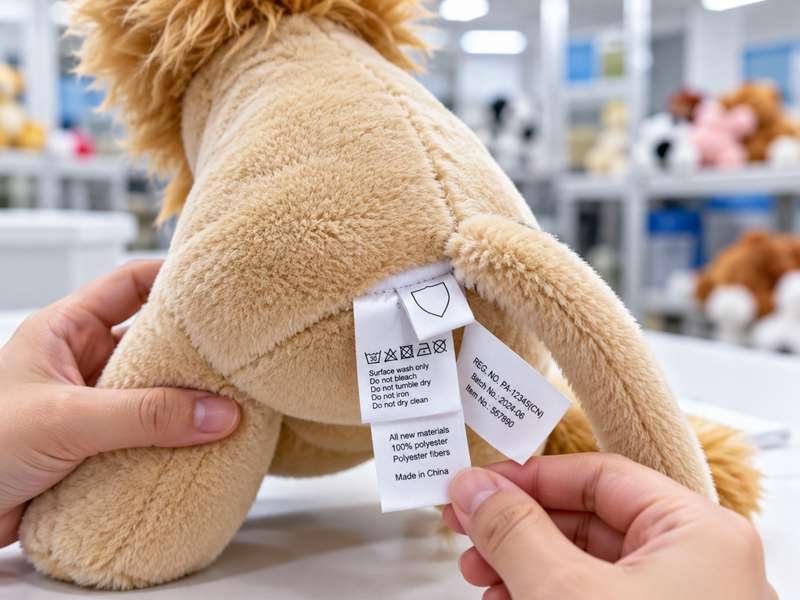
Labels & Wash Labels
Main labels, care labels, composition labels, warning labels, and traceability labels are part of the sellable product definition. Artwork revision, material, size, language, content, and sewing position must match the correct market and SKU.
- Control artwork revision and placement.
- Prevent old labels from entering a new production run.
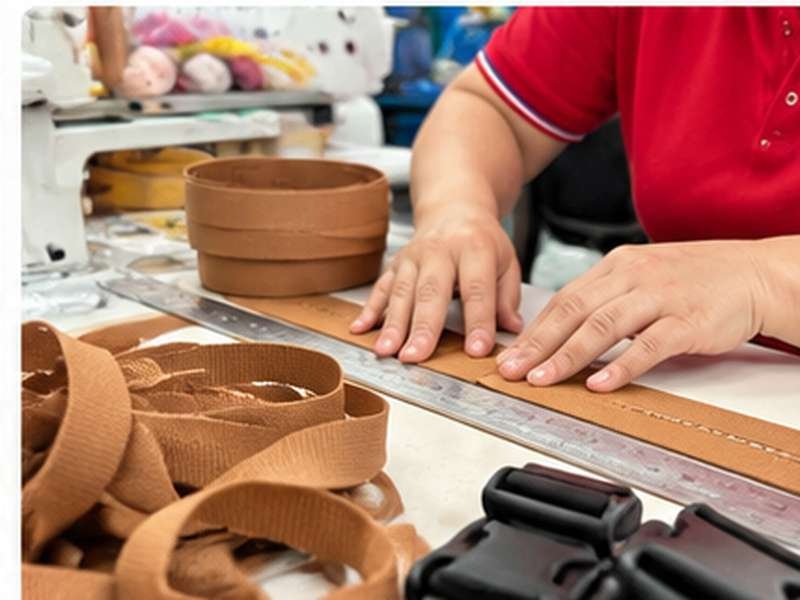
Ribbons & Elastic
Ribbons, elastic, hook-and-loop, webbing, cords, and similar trims can affect clothing fit, closures, hanging, adjustability, or decorative details. Width, stretch, color, construction, and fixing method should be defined where they affect repeated assembly.
- Specify dimensions and attachment.
- Check color and recovery when elasticity matters.
Hangtags & Consumables
- Tie retail components to packaging revision.
- Control consumables that affect visible finish or function.
Accessories and Components Engineered for Reliable Assembly
Hard parts and functional components need clear identity, fixing, safety, inspection, and packaging requirements before they enter bulk production.
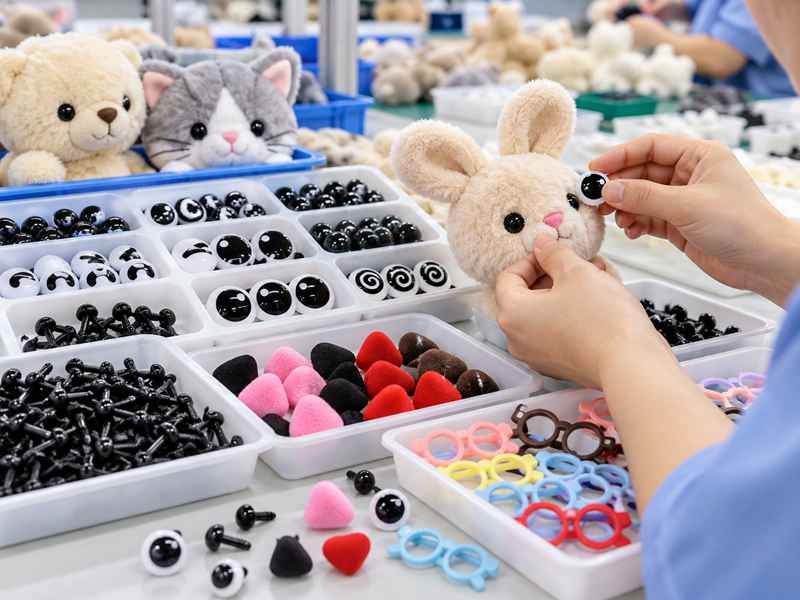
Plastic Eyes & Noses
- Control: part ID, size, fixing, position.
- Verify: pull, small-part, appearance, and applicable material requirements.
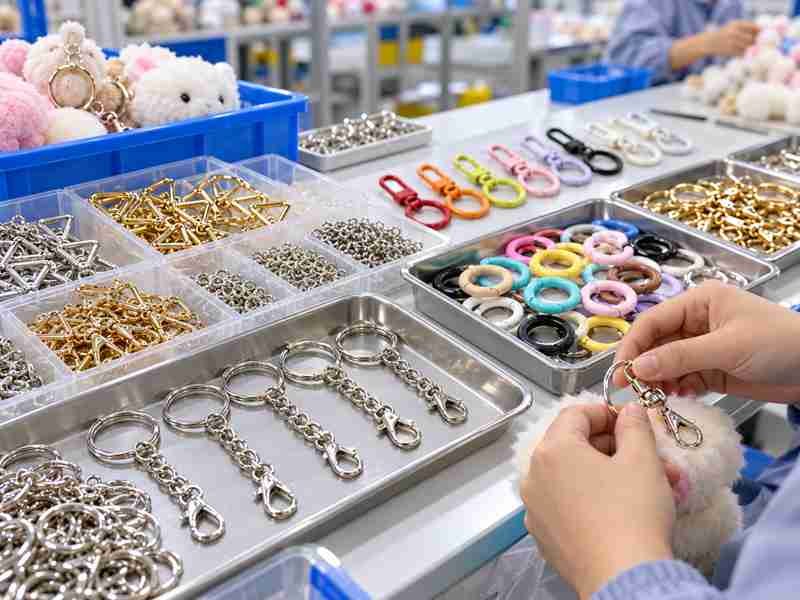
Metal Hardware
- Control: material, finish, size, attachment.
- Verify: strength, opening, edge condition, corrosion where required.
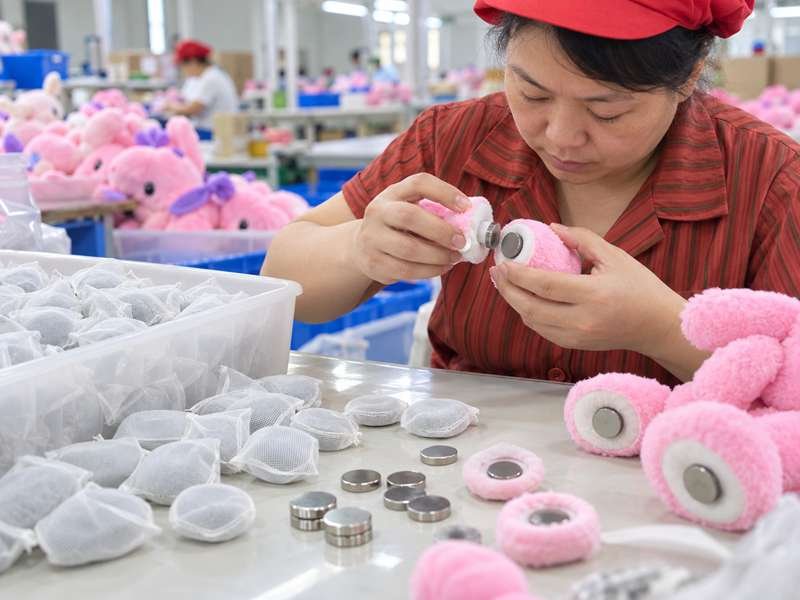
Magnets
- Control: magnet grade, location, polarity, retention.
- Verify: pull, internal security, function, applicable safety scope.
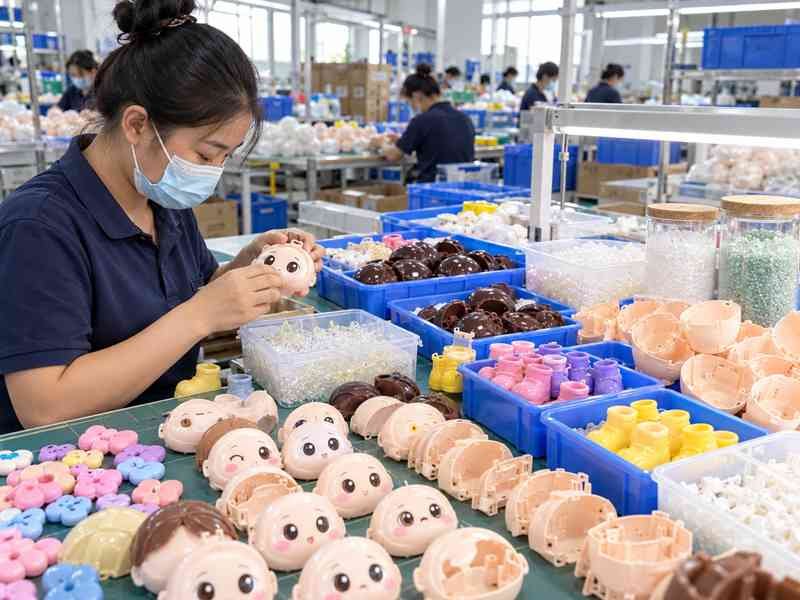
Plastic & Molded Parts
- Control: drawing, material, tolerance, finish, interface.
- Verify: fit, appearance, attachment, drop or impact where relevant.
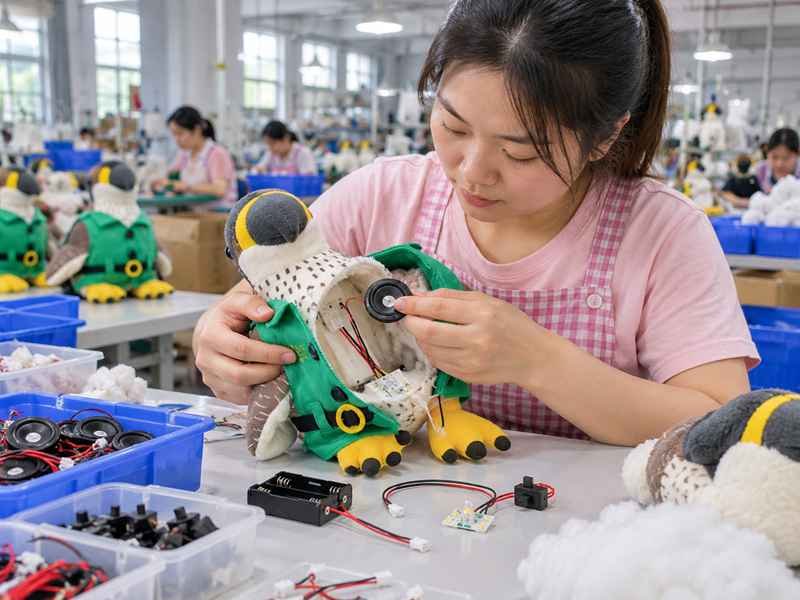
Electronic Modules
- Control: module revision and installation method.
- Verify: function, assembly, physical protection, applicable electrical scope.
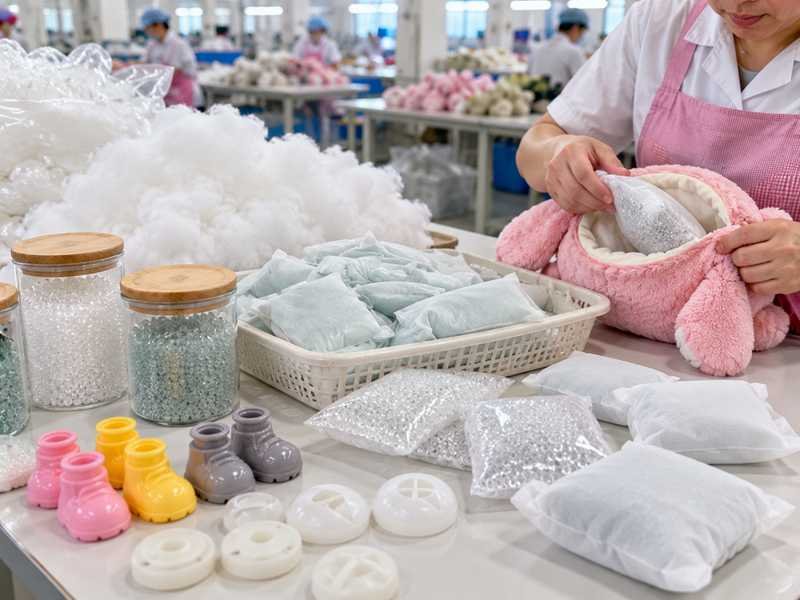
Filling & Structural Inserts
- Control: material, weight, zone, firmness.
- Verify: appearance, balance, containment, and approved handfeel.
Sample Development Connects Artwork to the Factory Floor
The Product Development Center turns visual intent into patterns, samples, materials, revisions, and production information before a SKU is scaled.
Review the Creative Input
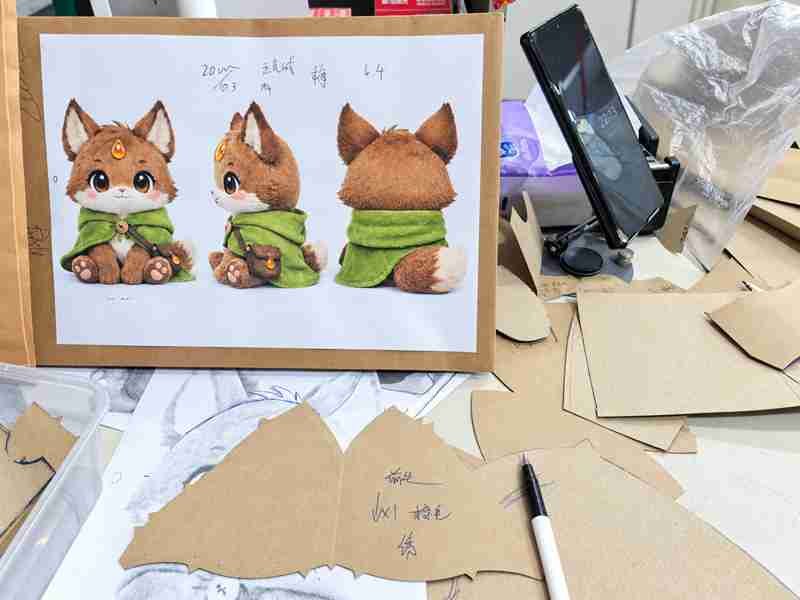
Development can begin with a hand sketch, 2D artwork, character sheet, three-view drawing, 3D render, AI-generated concept, reference product, or physical sample. The first task is to identify what is already defined and what the factory still needs to engineer.
Character review separates fixed visual DNA from flexible construction choices. Face shape, eye spacing, head-body ratio, pose, colors, clothing, logos, props, and signature details can be marked as high-priority references. Product use, target market, size, quantity direction, packaging, and launch timing are added because those commercial inputs can change materials and construction.
The result is a development brief with fewer hidden assumptions. Pattern work can then start from an agreed direction rather than trying to discover the product definition during sewing.
Engineer Pattern and Structure
Pattern engineering converts a visual design into panels, curves, seam routes, openings, grain or nap direction, and three-dimensional volume. Structure engineering deals with balance, internal support, cavities, hard components, magnets, electronics, weighted inserts, clothing, and any feature that cannot be defined by surface artwork alone.
The development team reviews whether panels can be cut repeatedly, seams are accessible, small parts have enough working space, turning openings are realistic, and later assembly can be performed without damaging previously completed work. Where a design contains extreme curves or rigid parts, sample construction can be adjusted before the factory commits to bulk tooling or materials.
Good pattern development is therefore not only about creating the first sample. It is about creating a structure the sewing and assembly teams can reproduce at production scale.
Validate Materials and Decoration
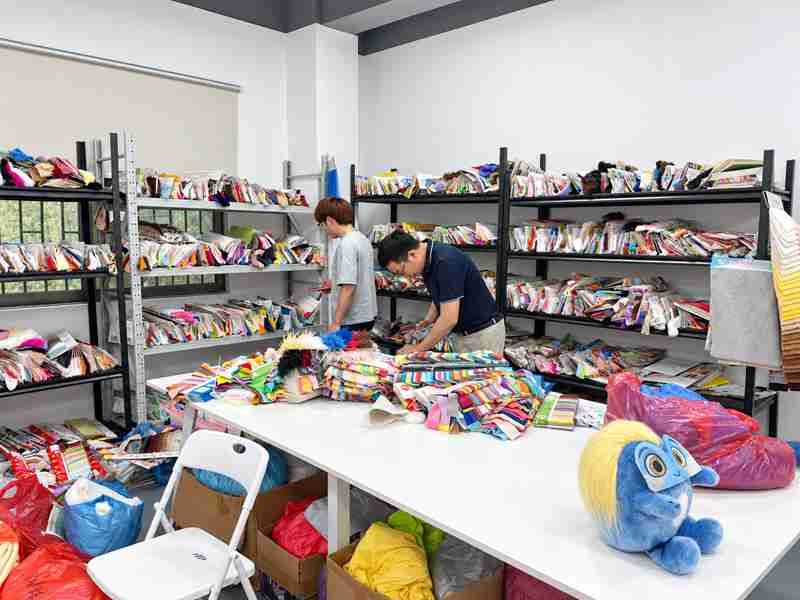
Fabric, color, pile height, nap, filling, embroidery, print, applique, clothing, hardware, and other components all influence how a character reads in three dimensions. Ewin develops those choices around the product rather than approving isolated swatches that may behave differently after cutting, sewing, stuffing, or packaging.
Material samples can be tied to GSM, pile, color, supplier route, and approved swatch. Decoration samples can record artwork revision, size, placement, thread or ink color, backing, and process. Accessories can be identified by part ID, material, size, color, weight, fixing method, and installation note.
Once the physical combination is approved, those details can move into the controlled BOM and production references instead of remaining as informal sample-room knowledge.
Control Samples and Documentation
A sample must be identifiable if its decisions are going to survive into production. Prototype, V1, revision, material, test, PP, and Golden Sample stages should not be mixed under labels such as “latest sample.” Each meaningful revision can record what changed and what remains approved.
Development documentation connects the physical sample to pattern, materials, colors, decoration, dimensions, filling, accessories, labels, packaging, cost impacts, and approval status. The Golden Sample then becomes the physical reference while the frozen BOM and released files carry details the sample alone cannot show.
That combination allows production, sourcing, quality, and packaging teams to work from the same SKU definition. Sample development becomes a controlled factory input rather than a separate creative activity.
Sample Stages Close Different Production Questions
Each sample stage has a purpose, helping development move from feasibility to an approved product definition before bulk manufacturing begins.
Prototype
V1 Sample
Revision Sample
Material / Color
Testing Sample
PP Sample
Golden Sample
Production Release
Cutting and Decoration Protect Shape Before Sewing Starts
The front end of manufacturing controls panel geometry, pile direction, facial placement, and decoration accuracy before the product reaches the sewing line.
Cut Against the Released Pattern
Cutting begins with the current released pattern rather than a sample-room paper piece with unclear status. Pattern data identifies panel shape, seam allowance, notches, mirrored parts, openings, grain or nap direction, and other construction marks needed for repeatable bundles.
The factory infrastructure includes automated spreading, CNC fabric cutting, laser cutting, straight-knife and band-knife cutting, press cutting, vision or positioning systems, and CAD/marker support. The purpose of those tools is different: high-volume layout, complex contours, small parts, thick stacks, positional cutting, or efficient marker use.
Material behavior still matters. Long pile, stretch, printed positioning, direction-sensitive shine, and mixed fabric thickness can require different cutting routes. A correct pattern cut in the wrong direction can create visible mismatch after sewing, so material and pattern information must stay connected.
Control Nap, Bundles and Panel Identity
Plush fabric direction directly affects color appearance, texture, face expression, and the way seams disappear. Direction arrows and marker rules help maintain consistent nap across head, body, limbs, ears, clothing, and other panels where the character should read as one product.
After cutting, panel identity and bundle control reduce wrong-color, left-right, mirrored, missing, or cross-SKU mixing. Similar characters in a series can use nearly identical panels with only a color or embroidery change, so clear project, SKU, part, and quantity identification becomes more important as collections grow.
High-risk panels can also be checked for position, shape, print alignment, or visible defects before sewing. Finding a cutting problem before hundreds of shells are assembled is faster and less costly than correcting the same issue at final inspection.
Embroider and Print to Approved Coordinates
Faces, logos, text, markings, and character graphics need more than an artwork file. Embroidery should specify final size, position, thread color, program version, backing, density, and any pile-control method. Printing should define process, artwork revision, color, position, scale, substrate, and relevant curing or handling requirements.
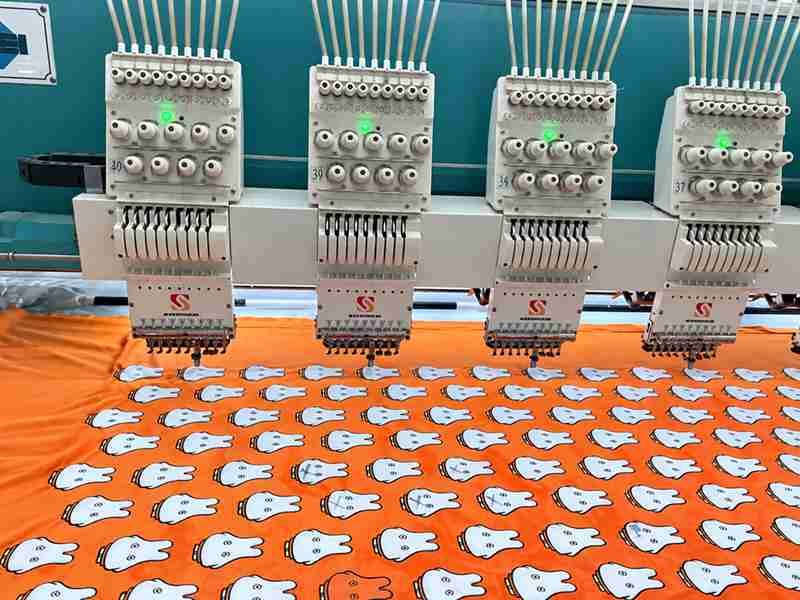
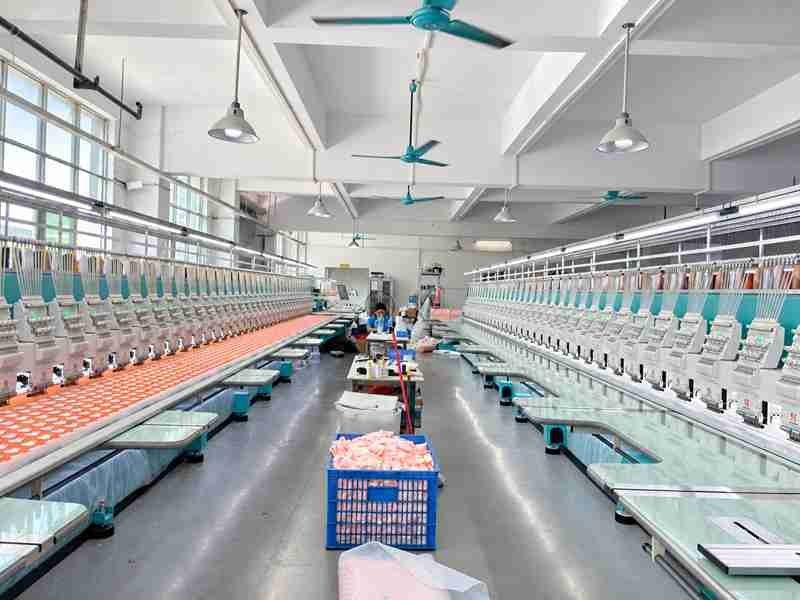
Ewin’s decoration infrastructure includes multi-head embroidery, small or irregular-part embroidery, embroidery digitizing, and heat-transfer capability alongside project-dependent print routes. First-piece confirmation helps verify expression and placement before bulk panels are processed.
Material choice changes the result. Long pile can bury stitches, stretch fabric can distort dense embroidery, and a printed color can read differently on another substrate. Decoration approval therefore belongs to the product and material combination, not to the artwork file alone.
Sewing and Assembly Turn Panels Into the Approved Product
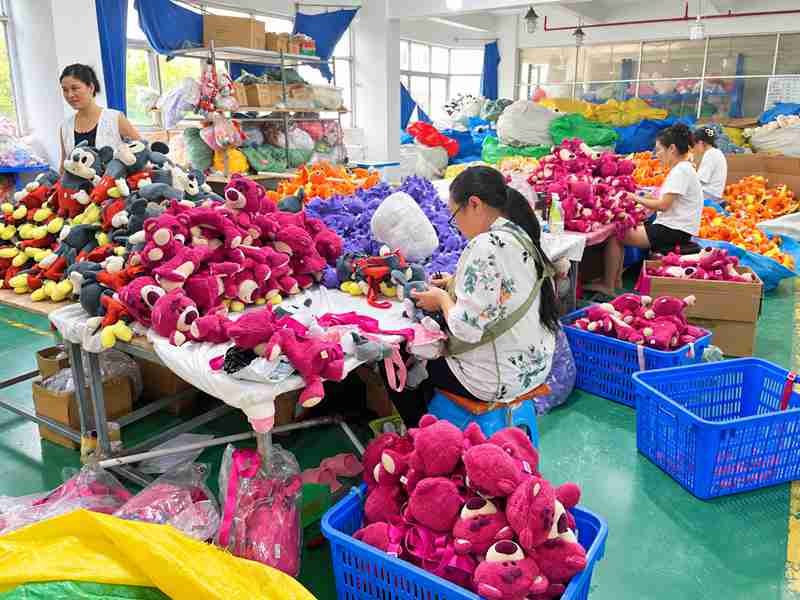
The production route controls structure, filling, manual detail, and finish so the approved sample can be repeated across a manufacturing batch.
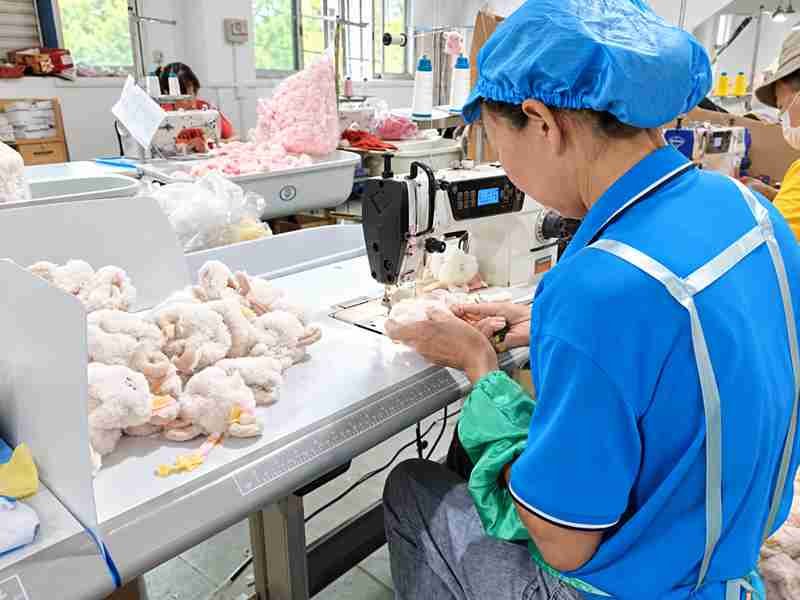
Sewing
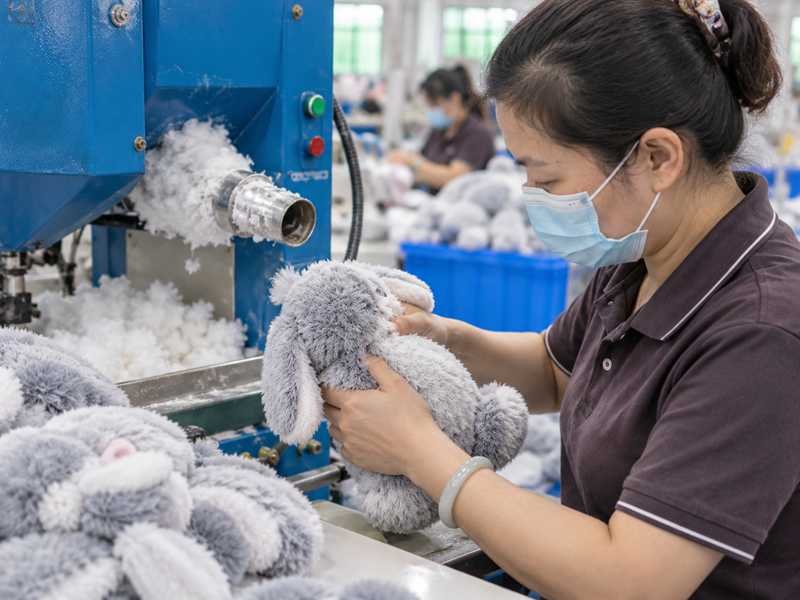
Stuffing
Shaping
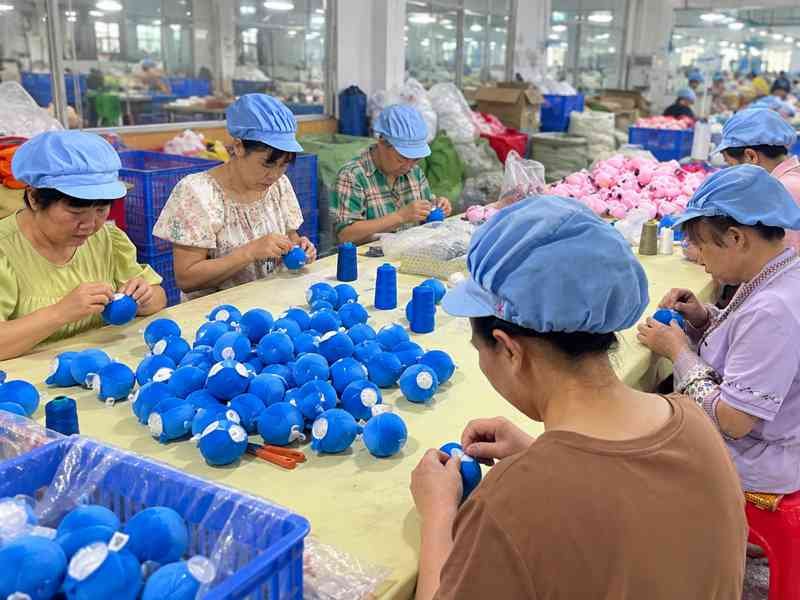
Closing
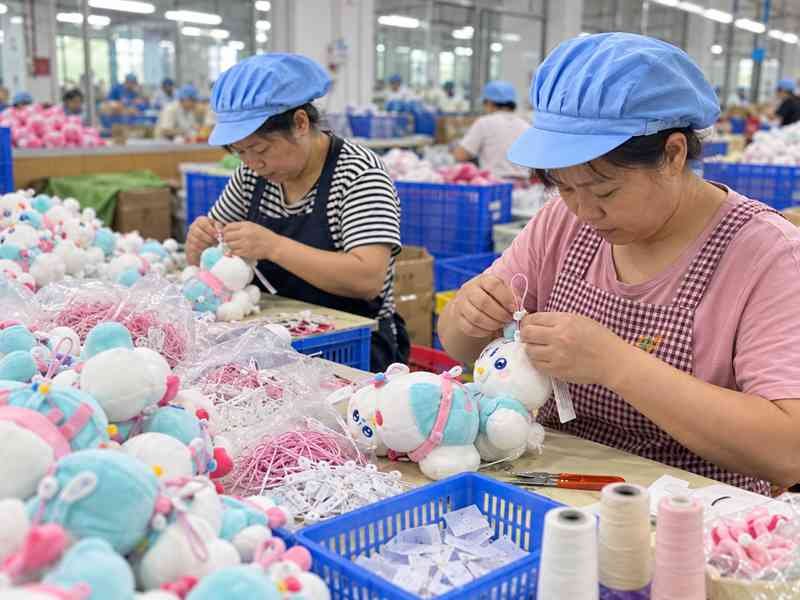
Accessory Assembly
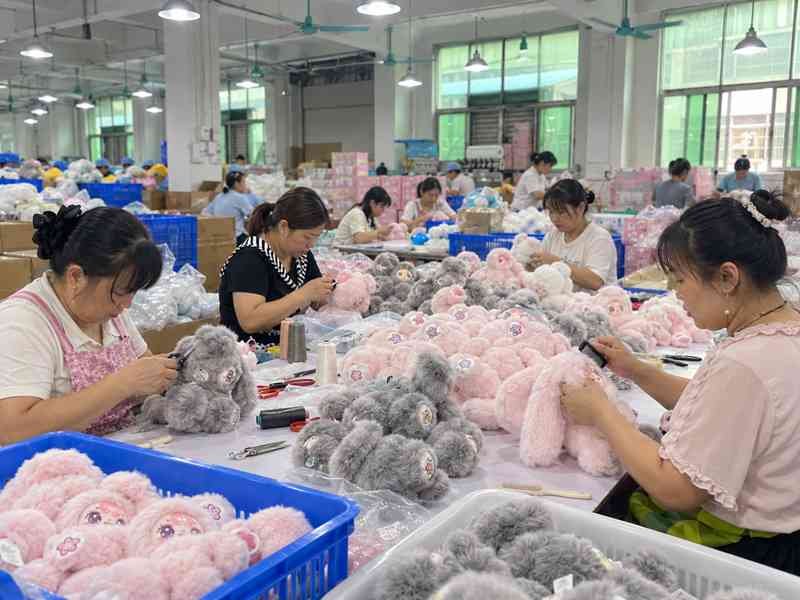
Finishing & Grooming
Bulk Production Starts From a Controlled Release
Mass production follows an approved product definition through material issue, manufacturing, in-process checks, finishing, and pack-out rather than scaling an informal sample.
Production Release
Material Issue
Cutting & Bundling
Decoration
Sewing & Assembly
IPQC & Finishing
Final Inspection
Final Pack-Out
Approved Samples Become Repeatable Production Standards
Physical approval, controlled data, and change management work together so bulk output follows the product version that was actually approved.
Golden Sample Defines the Physical Standard
The Golden Sample gives the factory a physical reference for proportion, silhouette, face, handfeel, filling, clothing, component location, decoration, and overall presentation. It should be clearly identified by project, SKU, revision, and approval status so it cannot be confused with V1, testing, sales, or obsolete samples.
A physical sample is powerful because operators and inspectors can see relationships that numbers alone cannot capture. However, it does not show hidden material codes, exact embroidery files, supplier route, filling weight, label artwork, or packaging instructions. For that reason, Ewin uses the physical reference together with controlled production data rather than asking the factory to “copy the sample.”
Where a project requires separate controlled samples, customer, factory, and QC references can be maintained so the same approved appearance is available at different decision points.
Frozen BOM and Released Files Define the Data
The frozen BOM records the materials and components behind the approved sample: fabric identity, composition, GSM, pile, color, thread, accessories, filling, labels, packaging, and other critical items. Released pattern and decoration files carry panel geometry, embroidery, print, dimensions, and process-linked information that the physical sample cannot communicate precisely.
BOM status should move from DRAFT to CONTROLLED to FROZEN as development matures. During early sampling, options can change. After approval, unrecorded substitutions should stop. If a later supply, cost, quality, or design change is needed, the impact can be reviewed before a new revision is released.
That discipline keeps purchasing, production, quality, packaging, and reorder teams from using different definitions of the same SKU.
Change Control Protects Later Production
A product rarely stays unchanged forever. A new supplier, different fabric lot, revised accessory, updated label, packaging change, electronic module revision, or cost optimization can affect appearance, testing, assembly, lead time, or commercial approval. The important point is not to forbid change; it is to stop silent change.
A controlled change identifies what is changing, which SKU and version are affected, whether a new sample or test is needed, which documents must be updated, and who approves the release. The revised Golden/BOM/pattern/artwork relationship should remain clear after the change.
Reorders can then use a delta review: reuse proven production information, check what changed since the prior run, and carry forward previous defect or CAPA learning rather than restarting from memory.
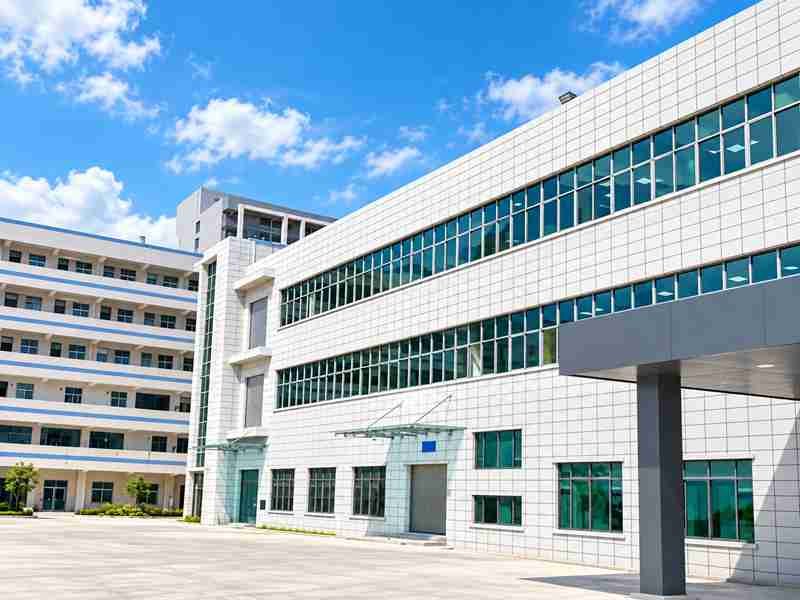
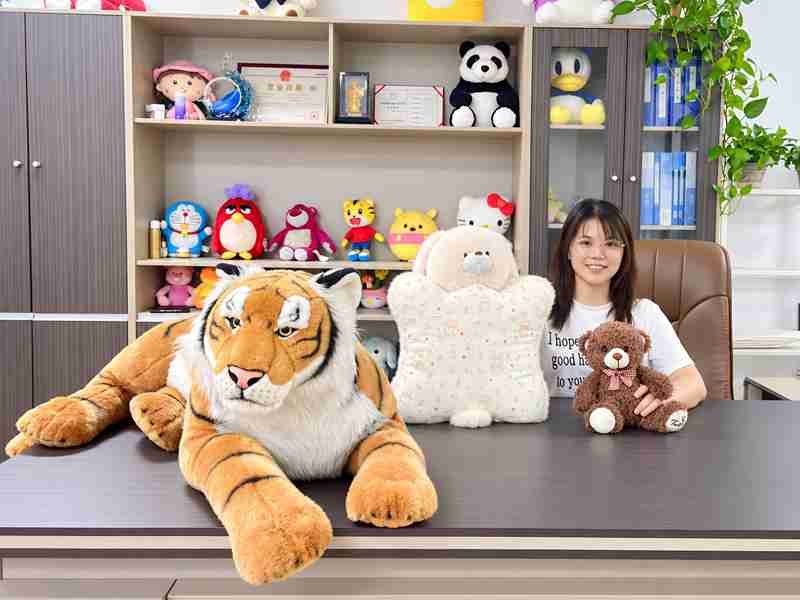
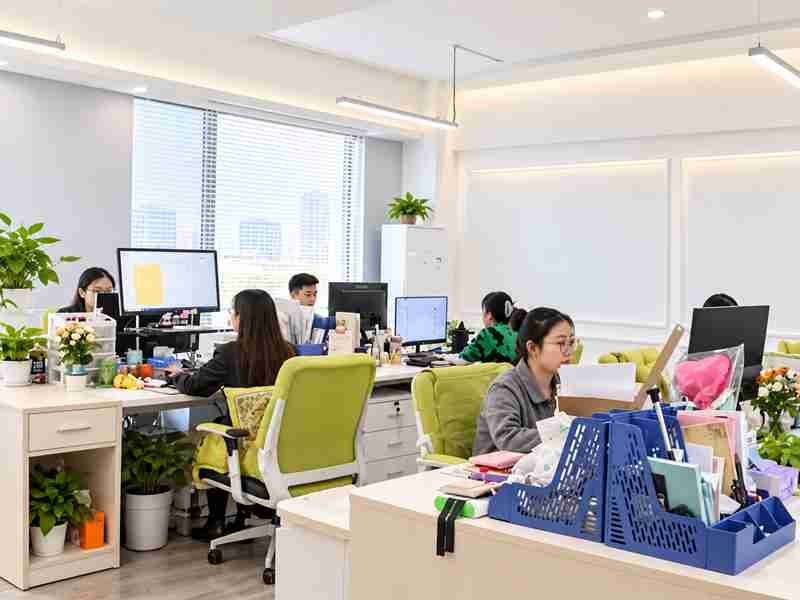
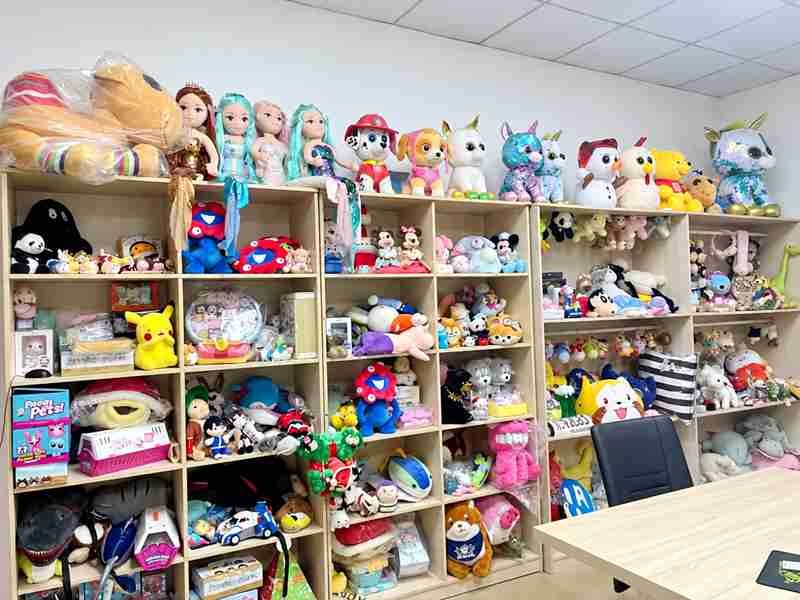
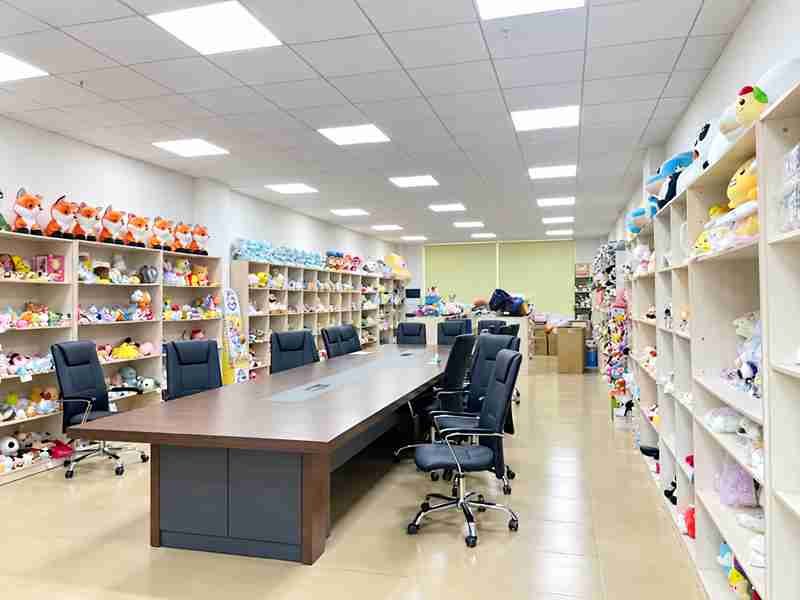
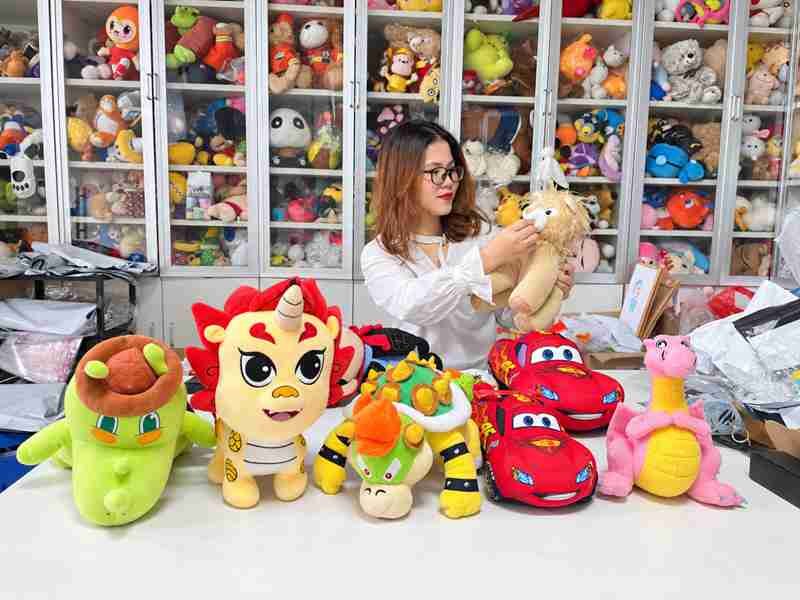
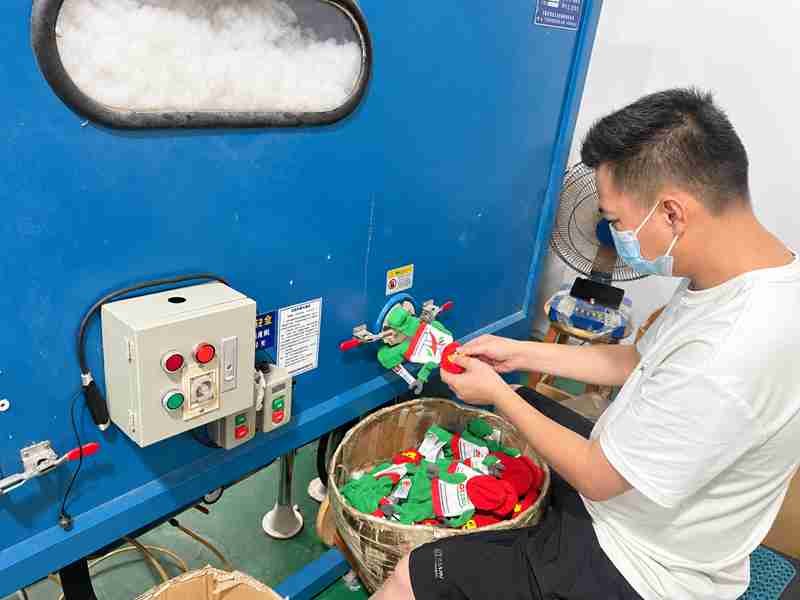
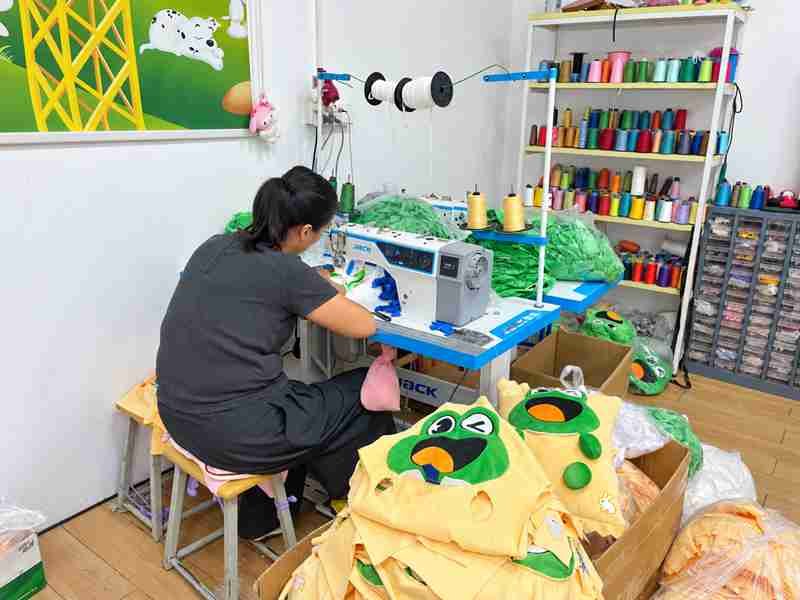
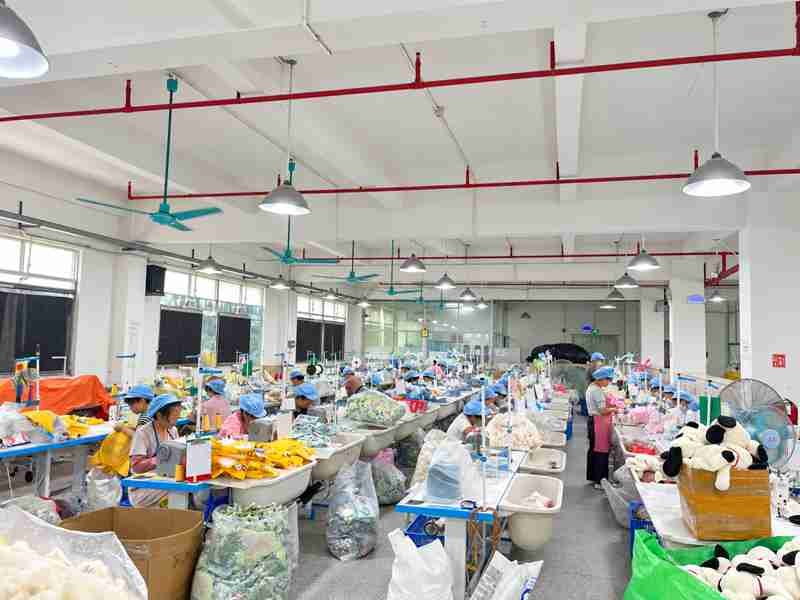
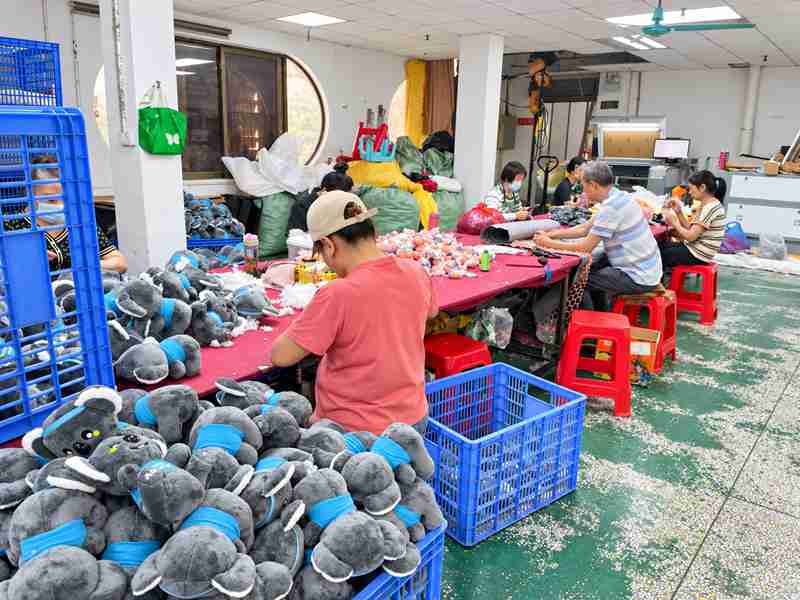
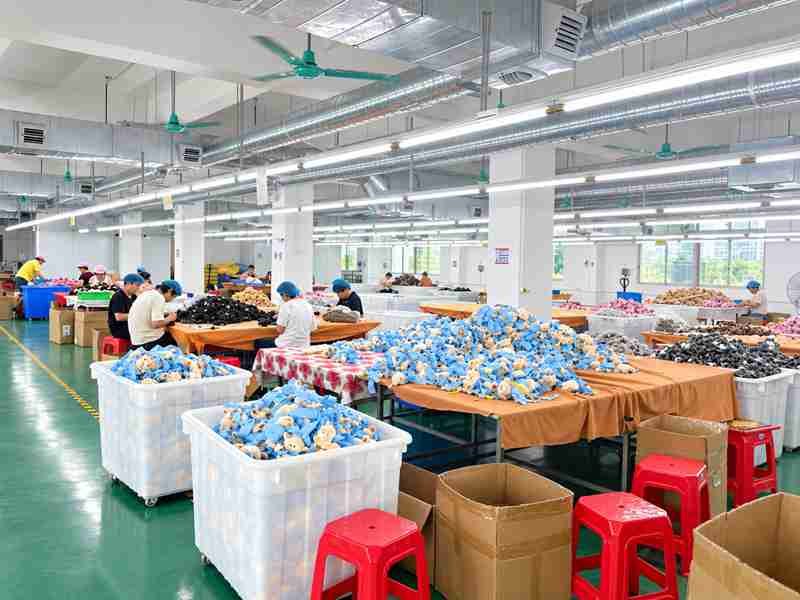
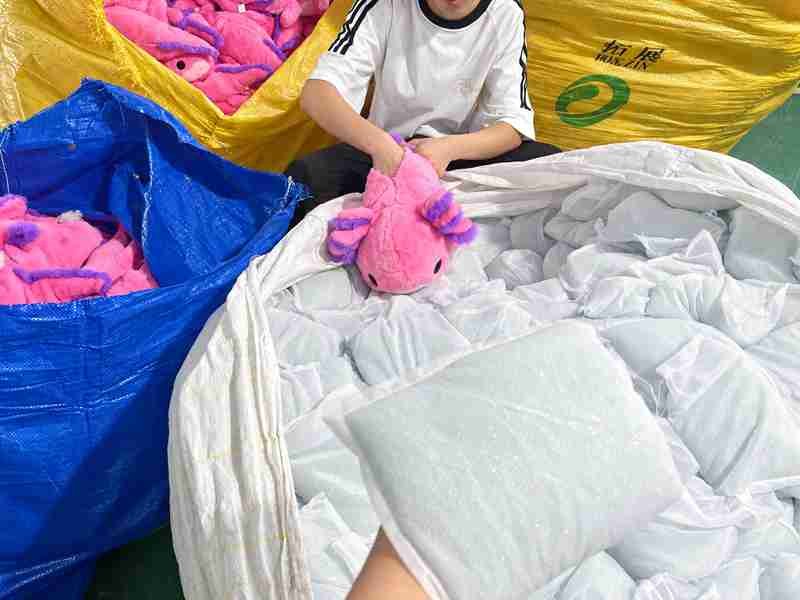
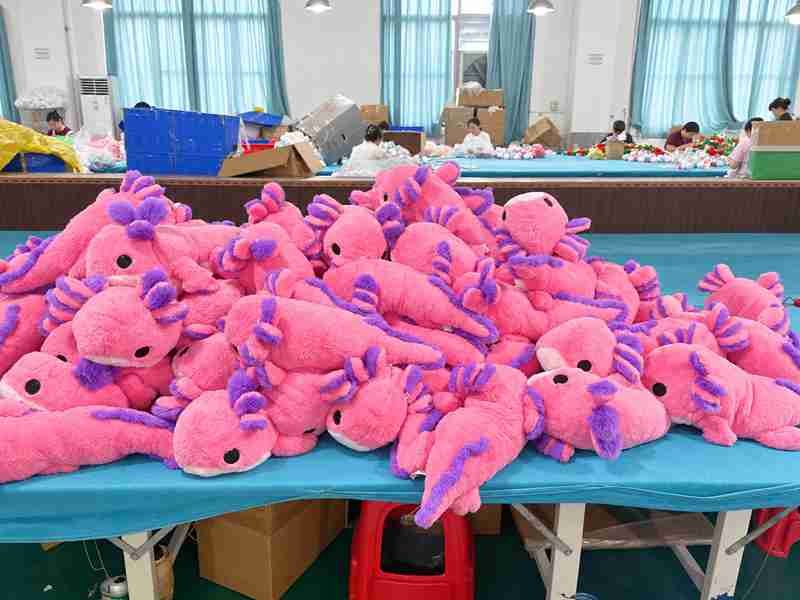
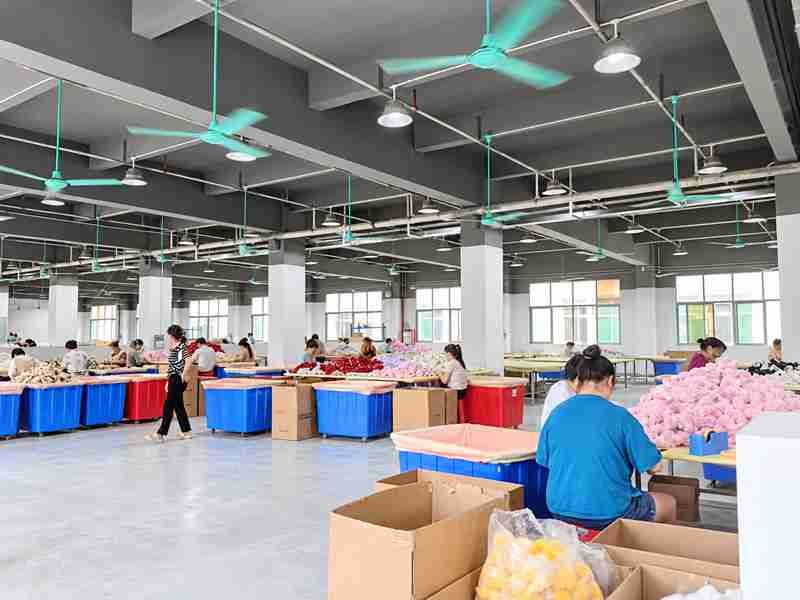
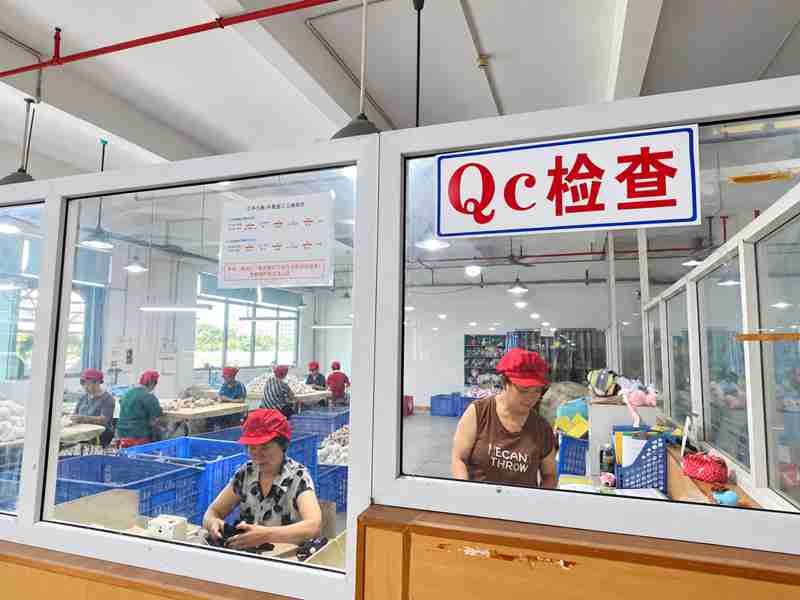
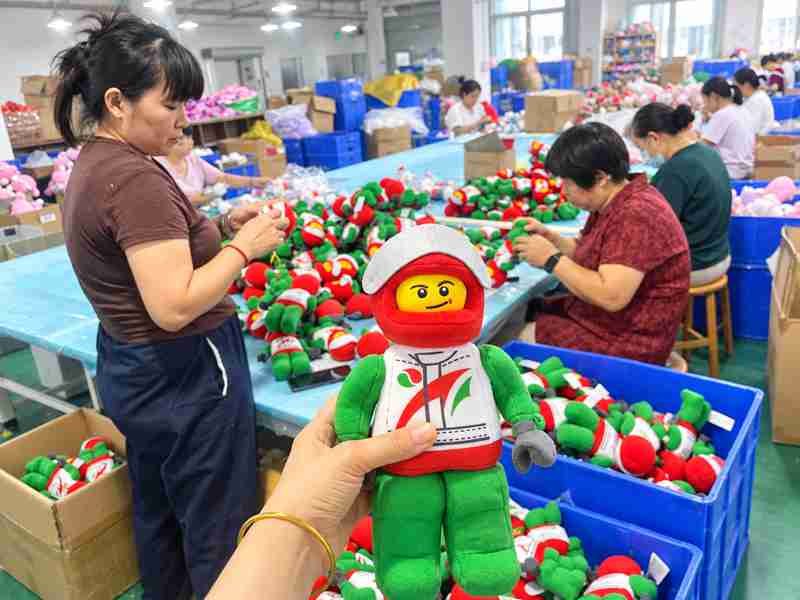
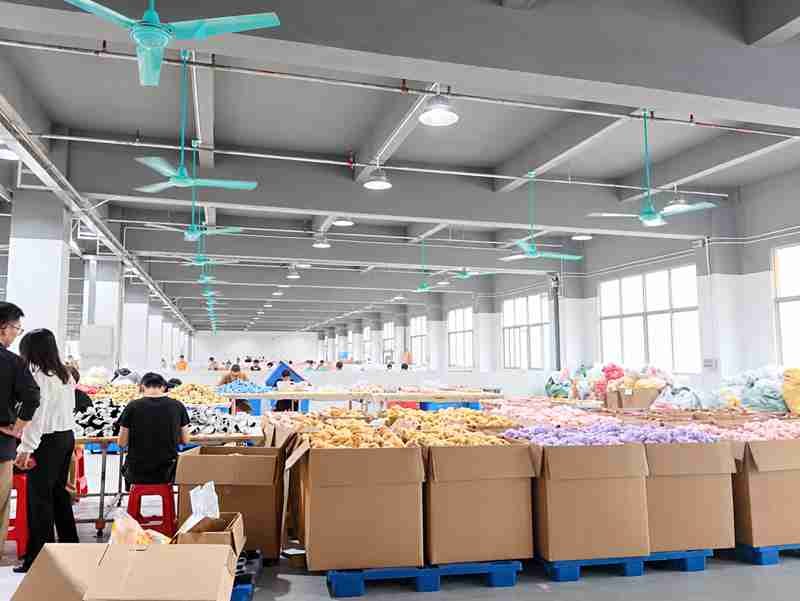
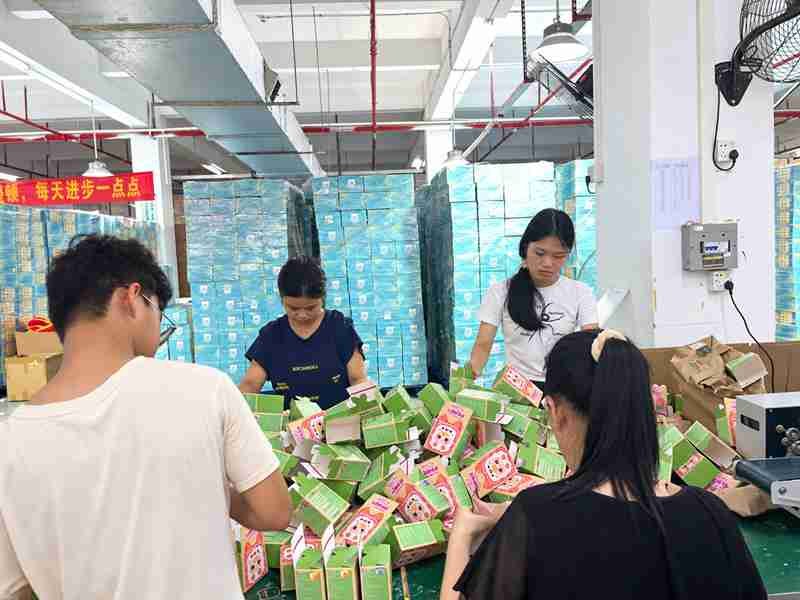
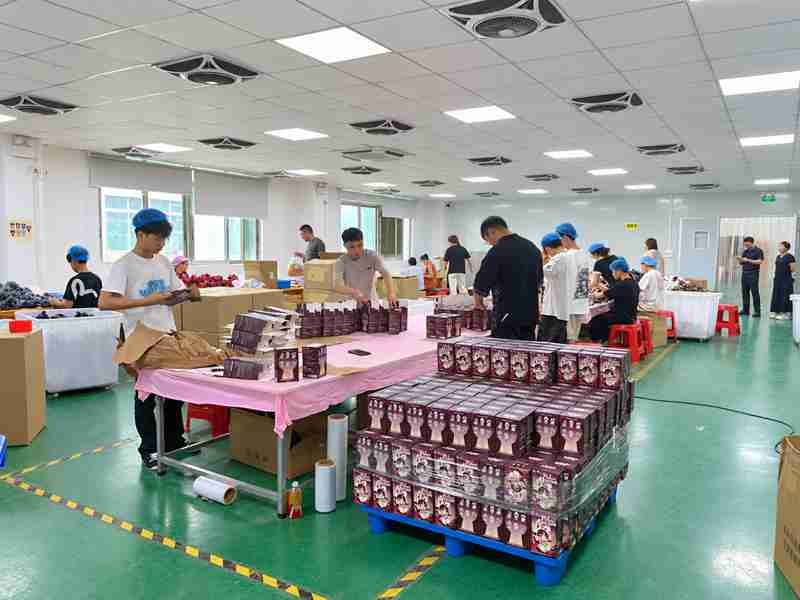
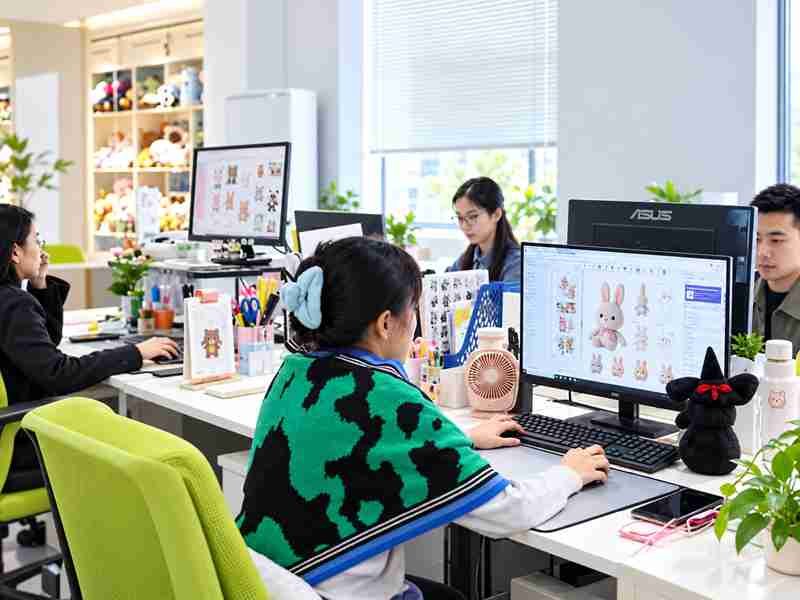
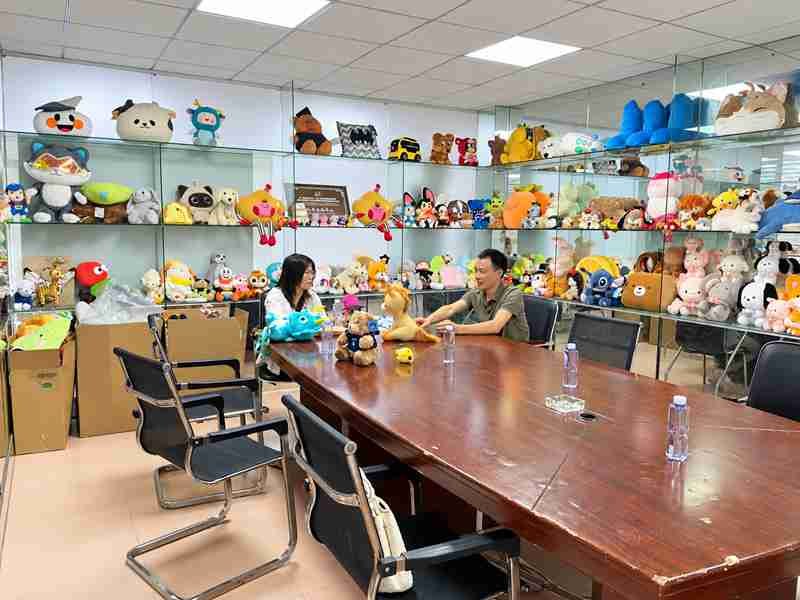
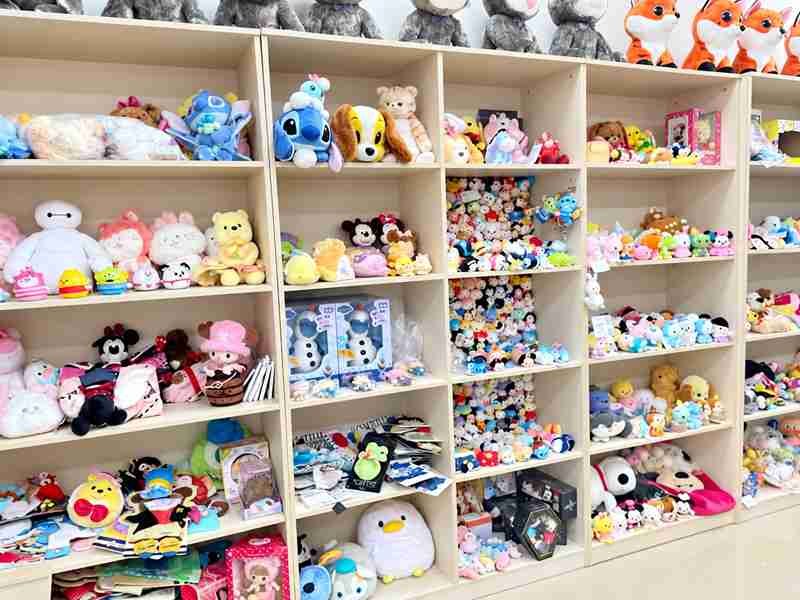
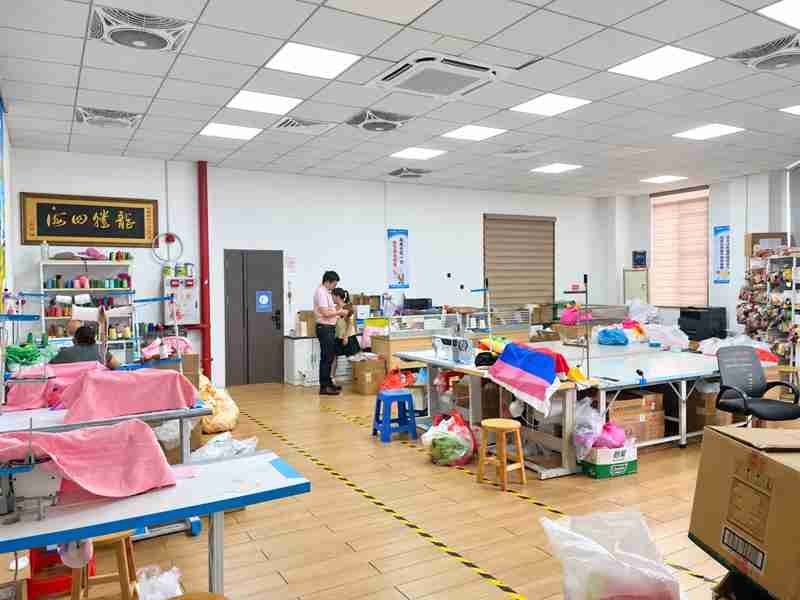
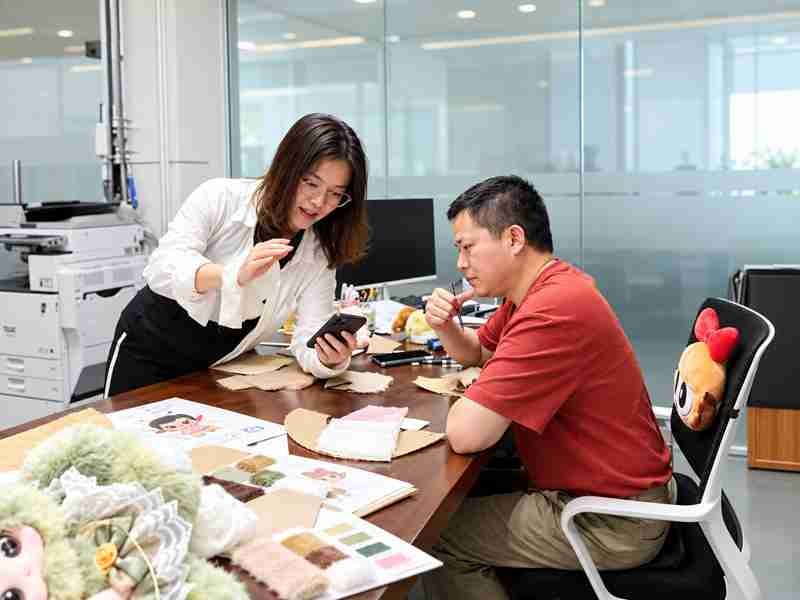
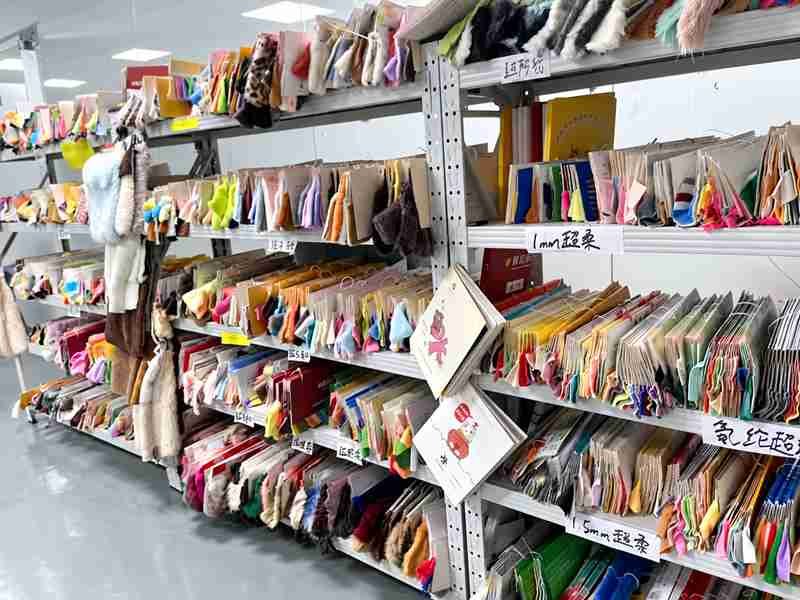
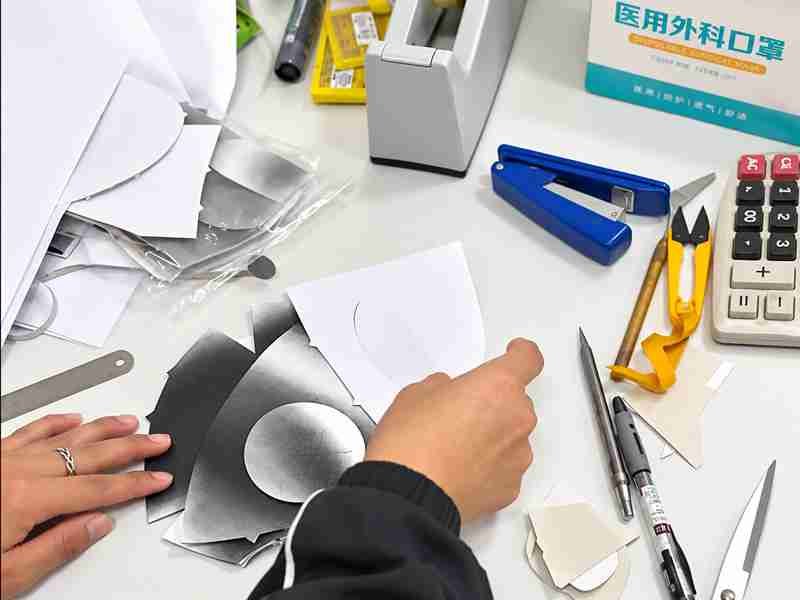
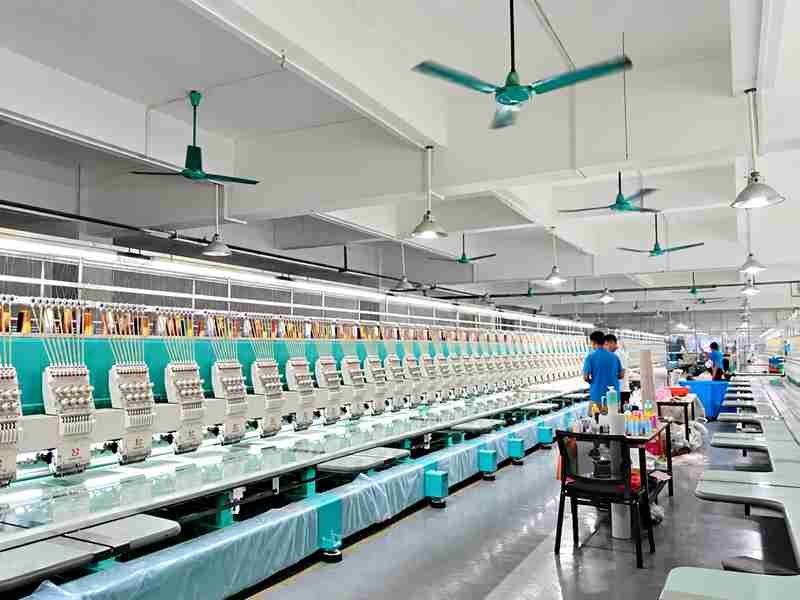
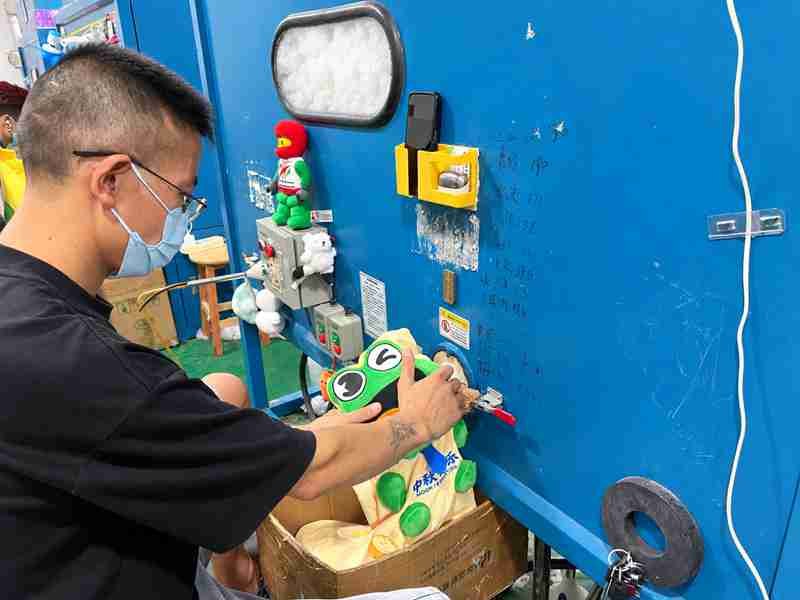
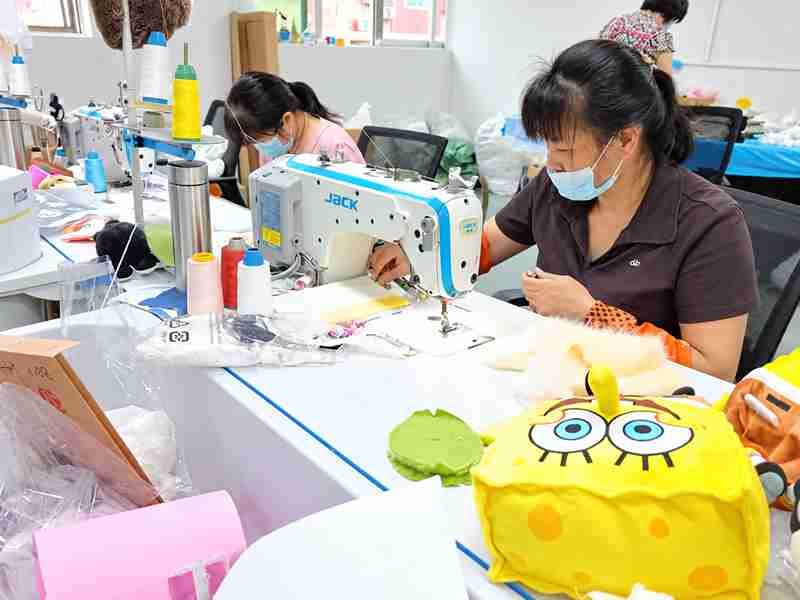
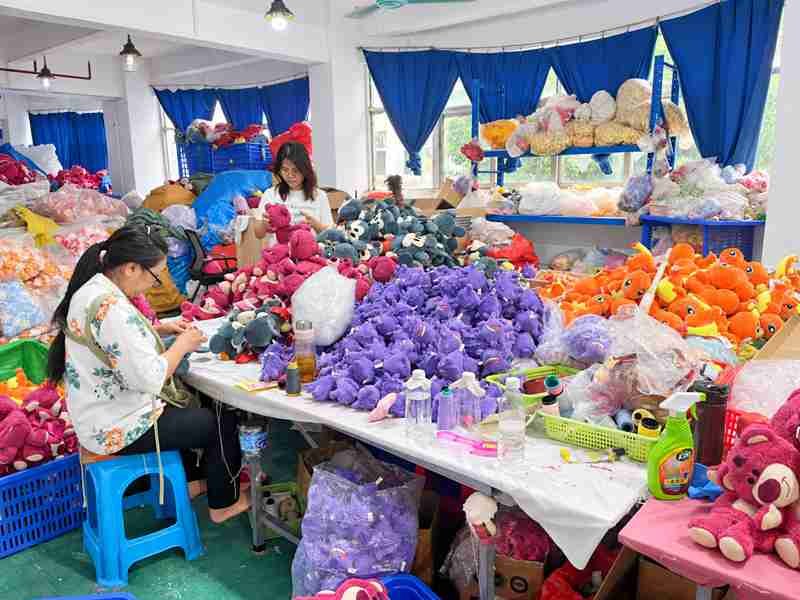
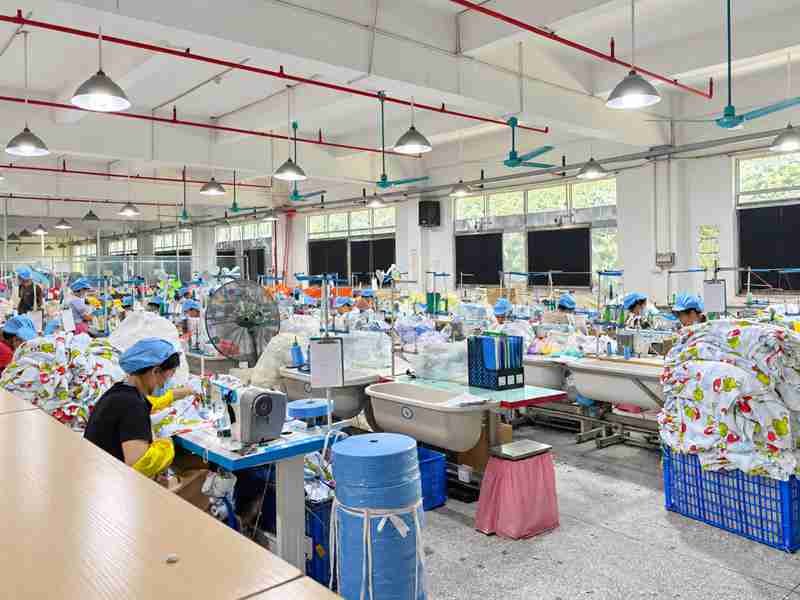
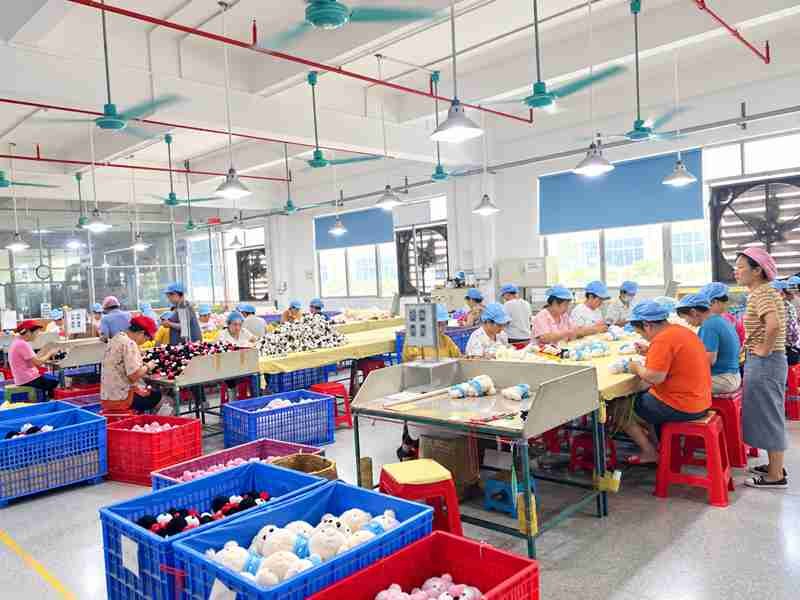
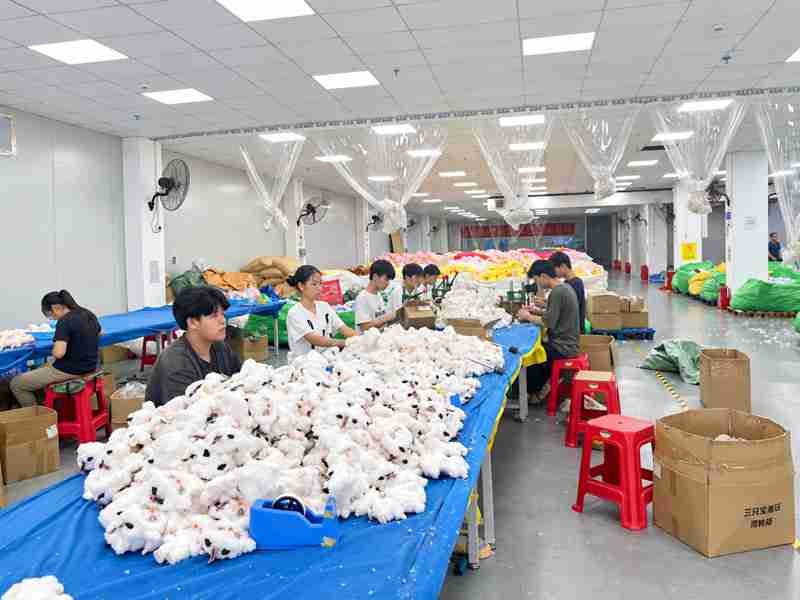
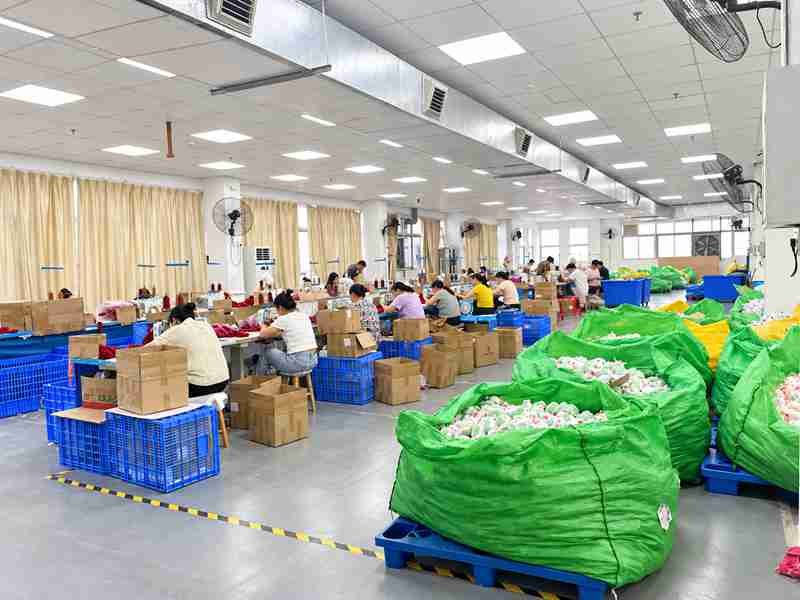
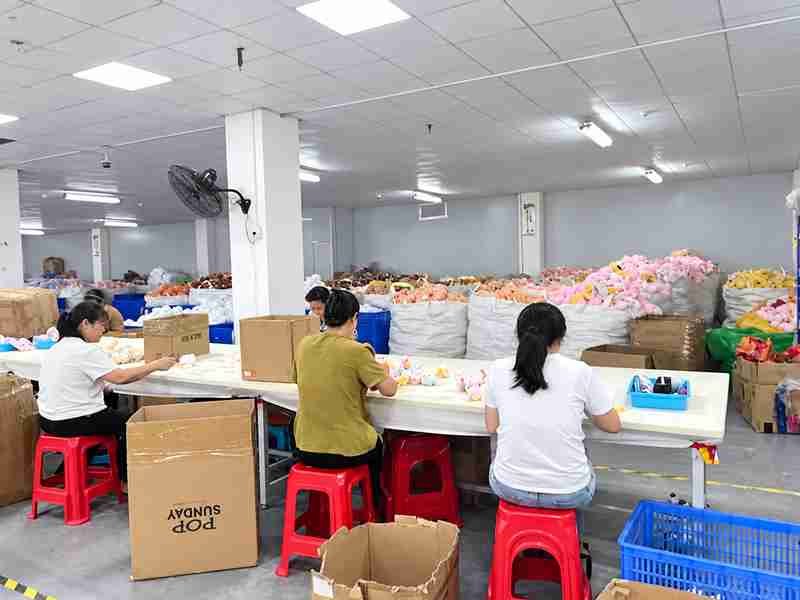
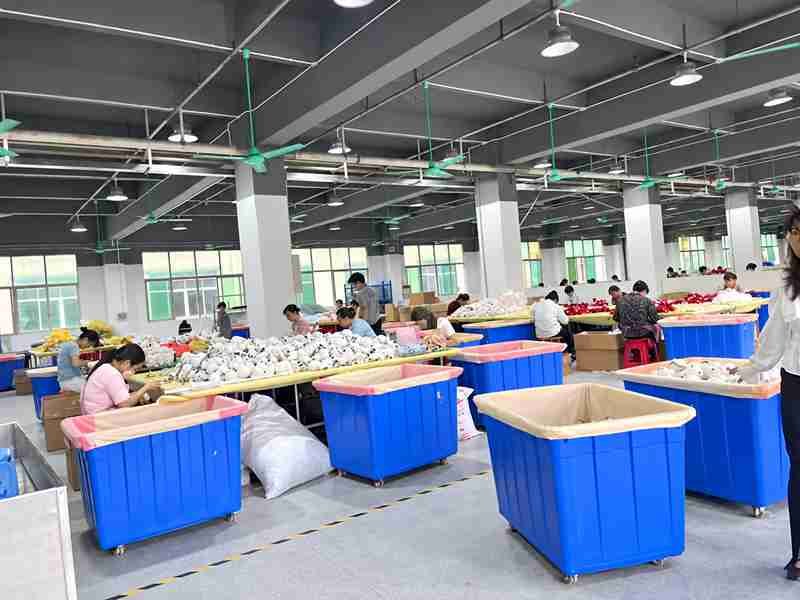
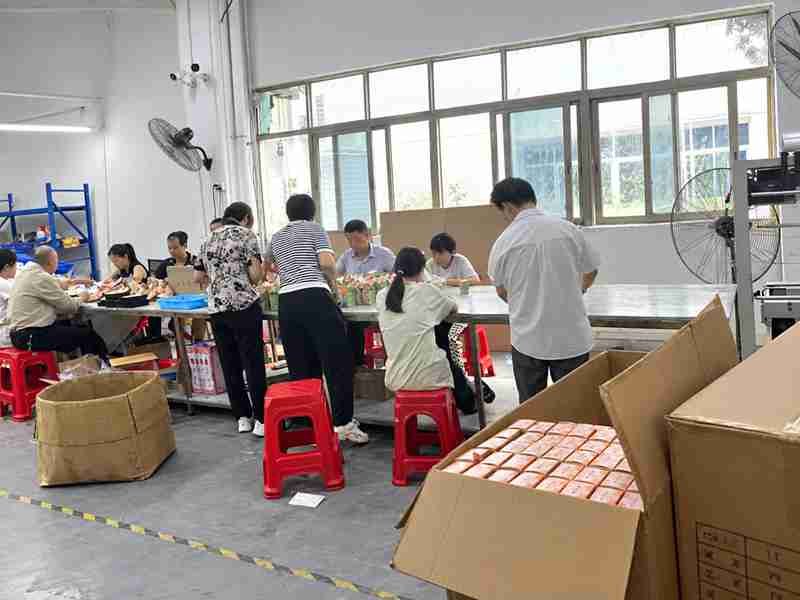
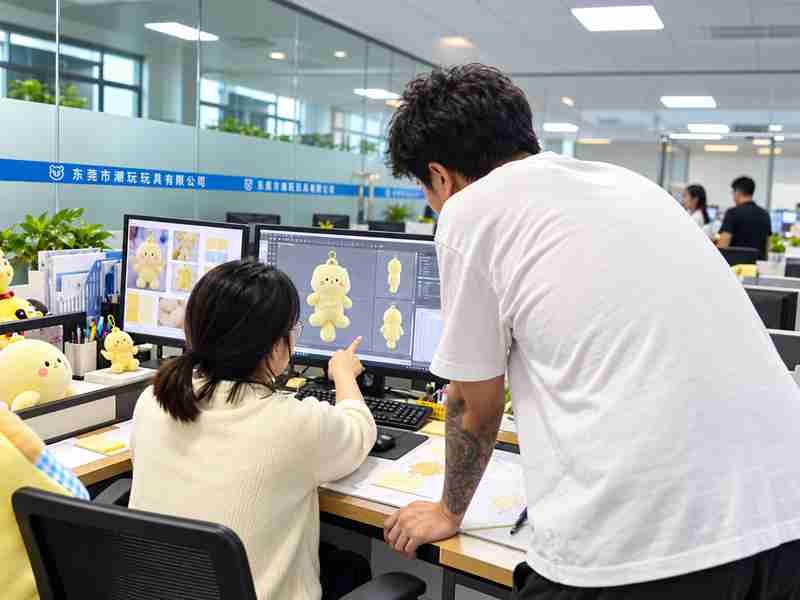
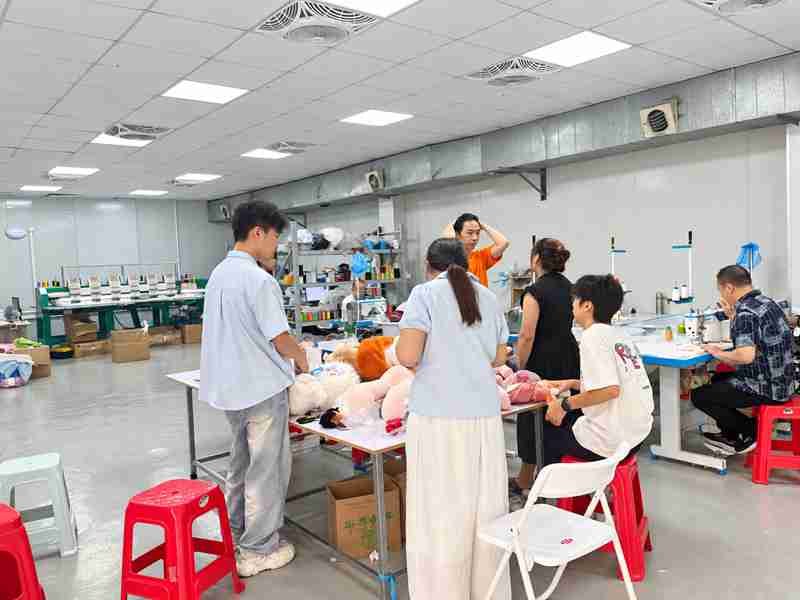
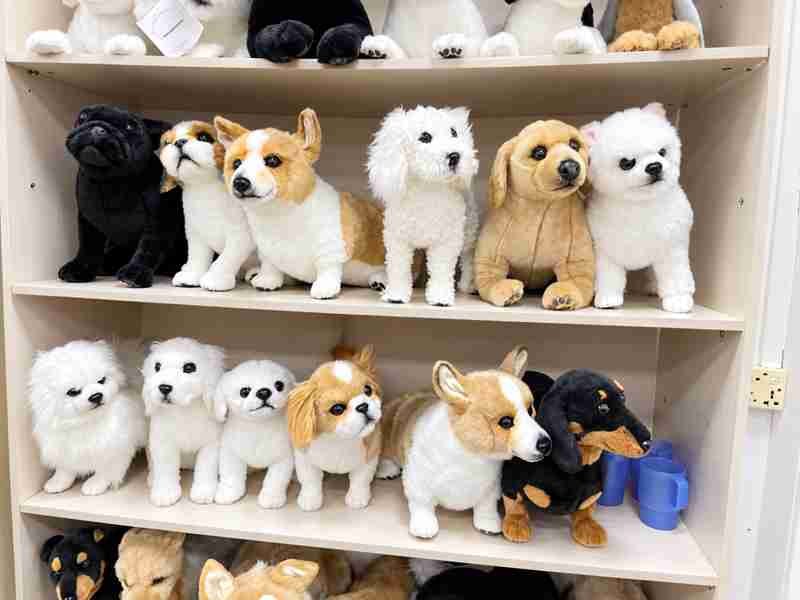
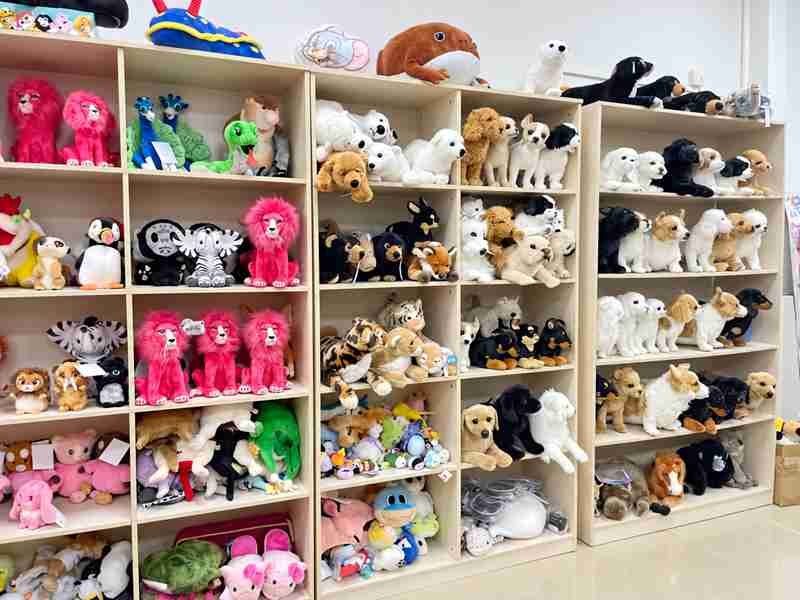
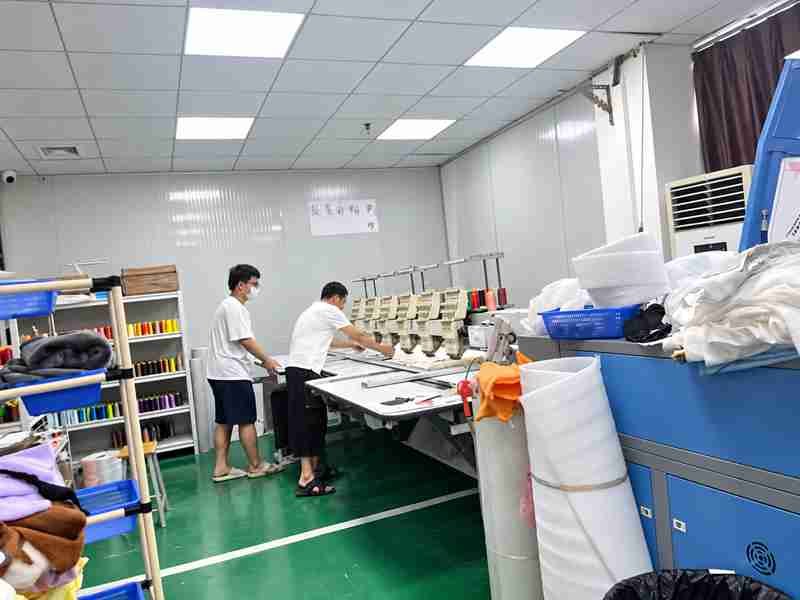
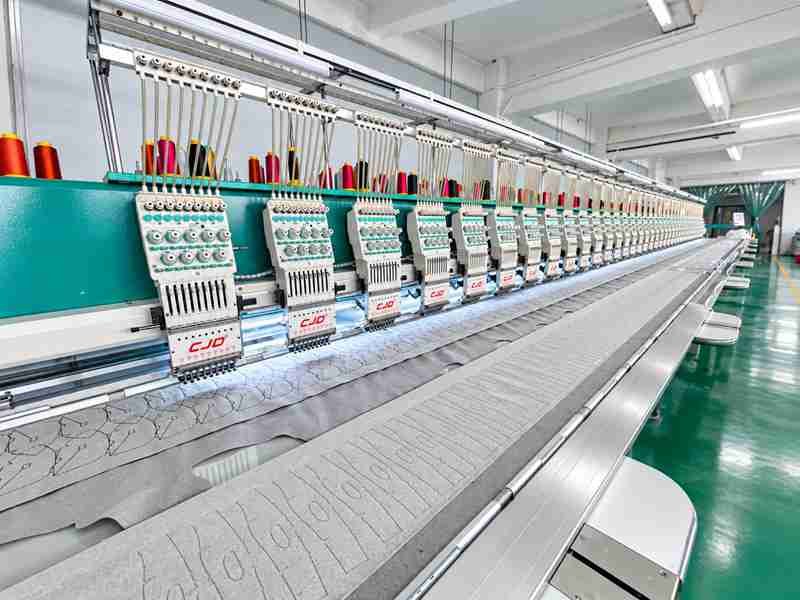
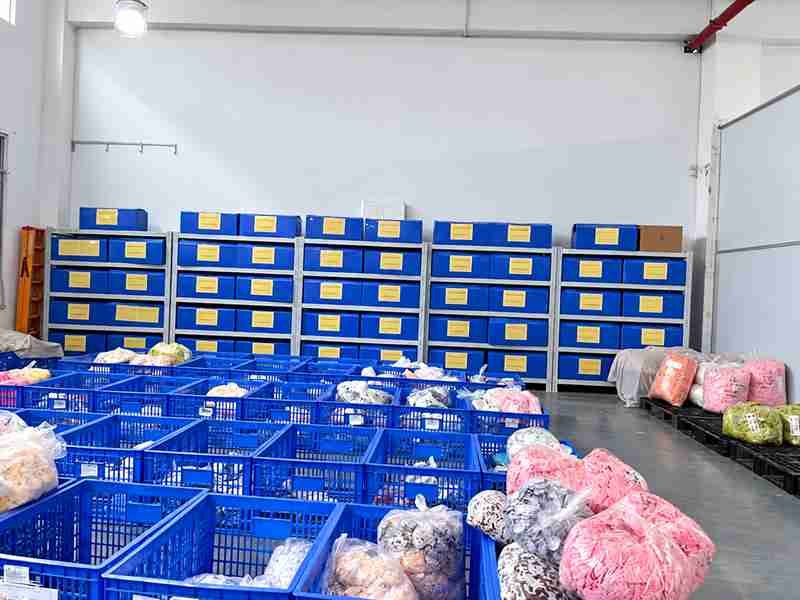
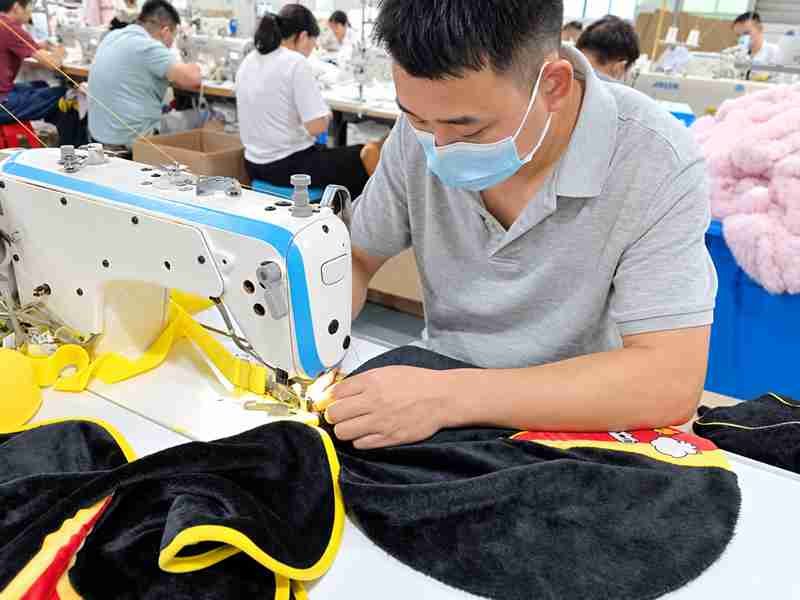
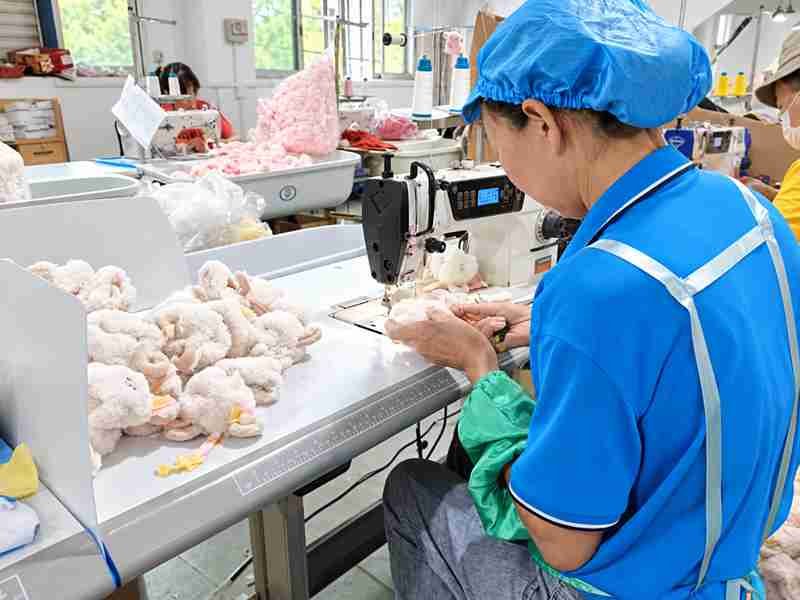
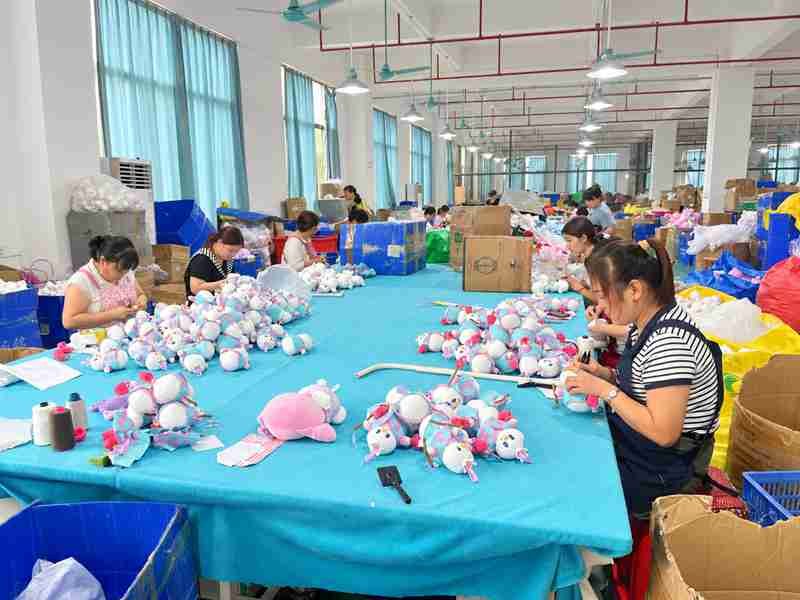
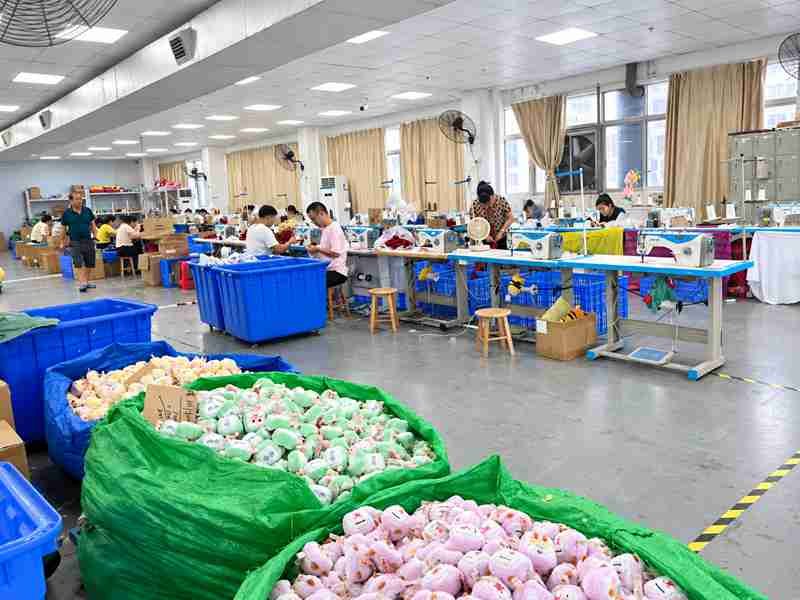
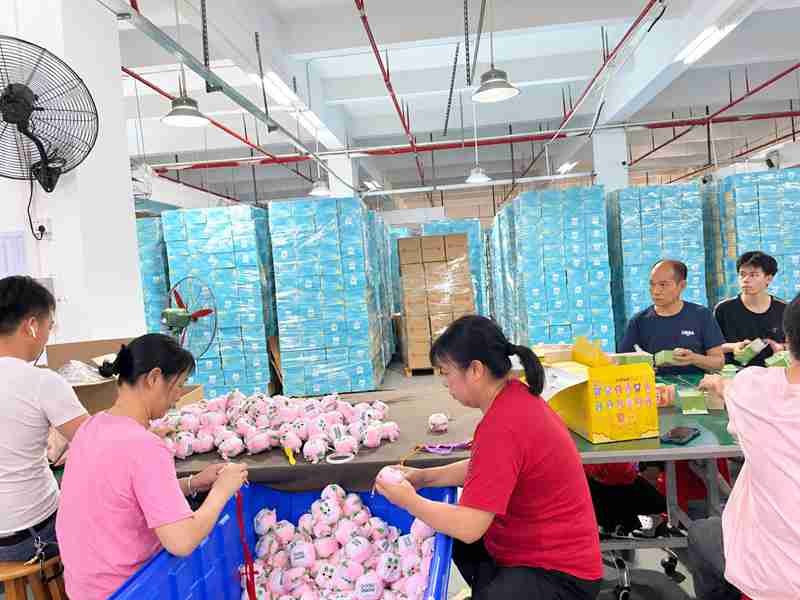
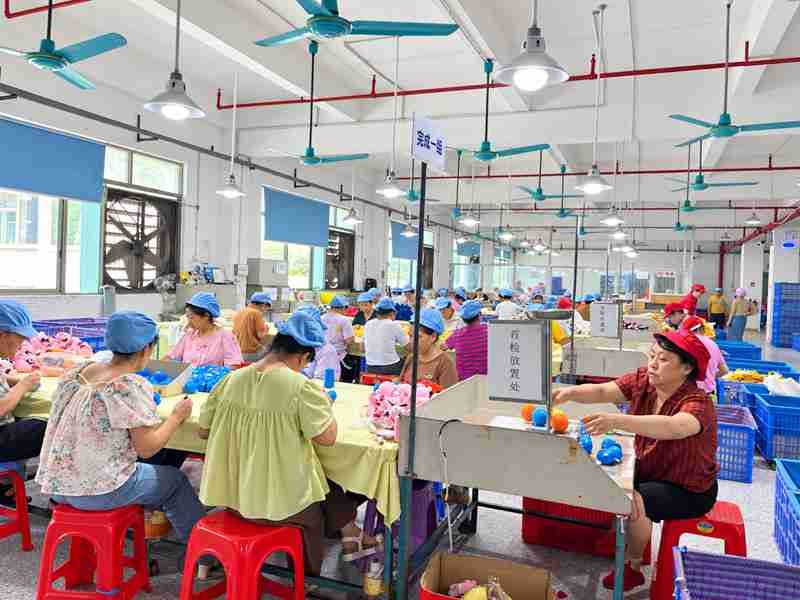
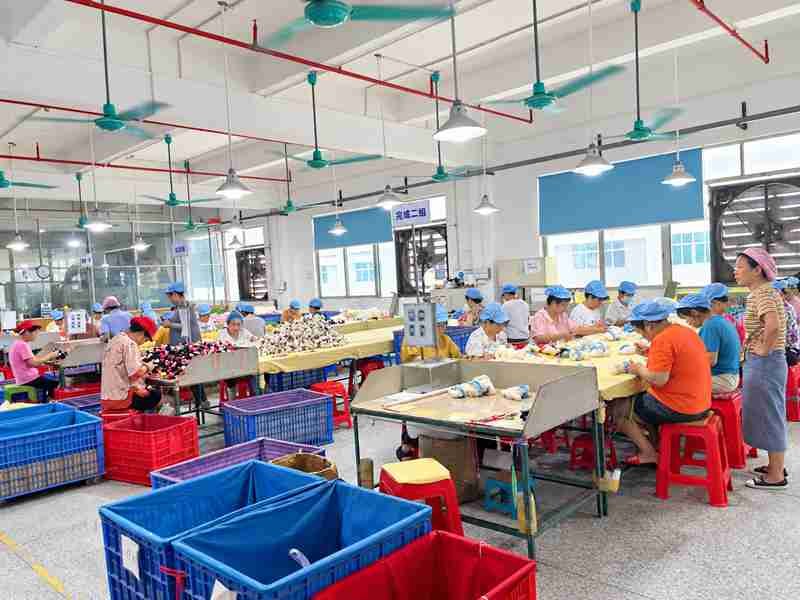
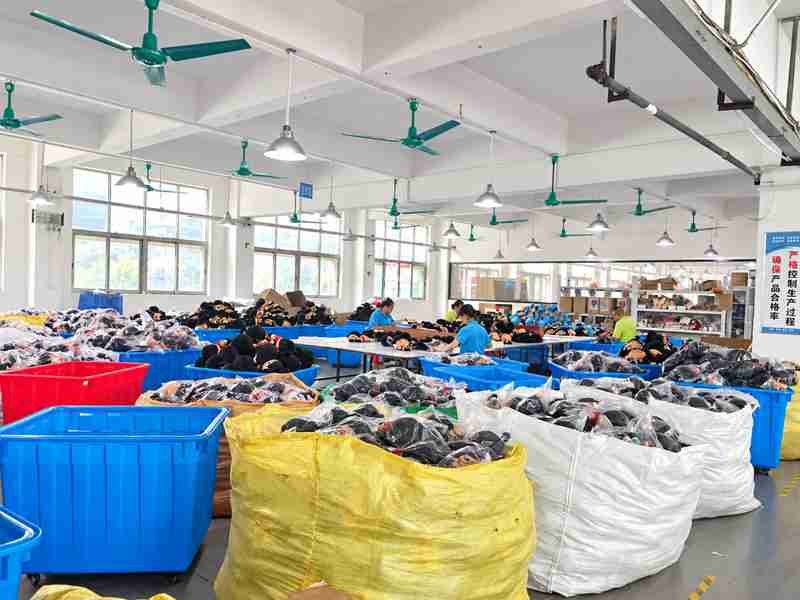
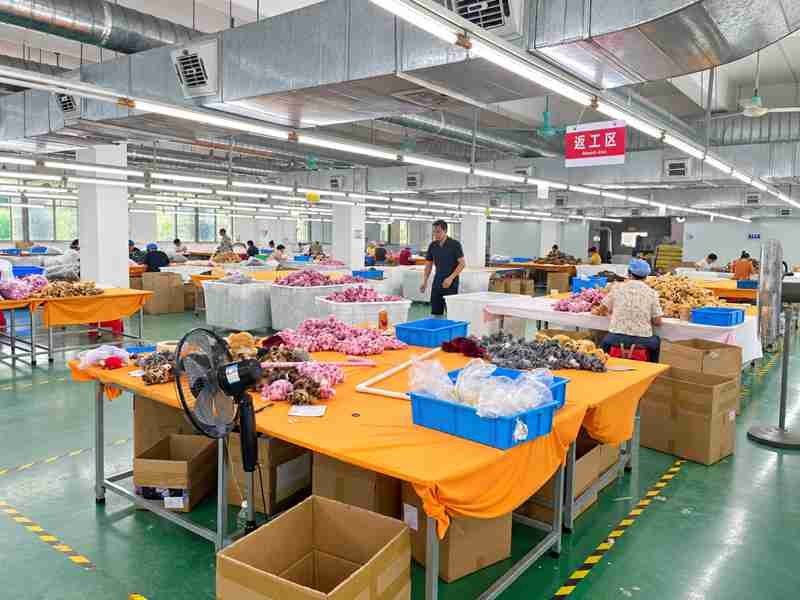
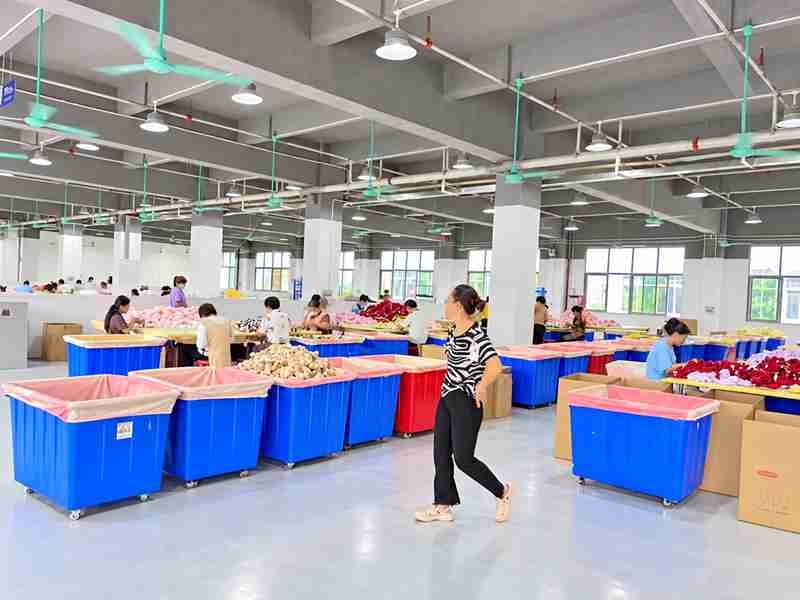
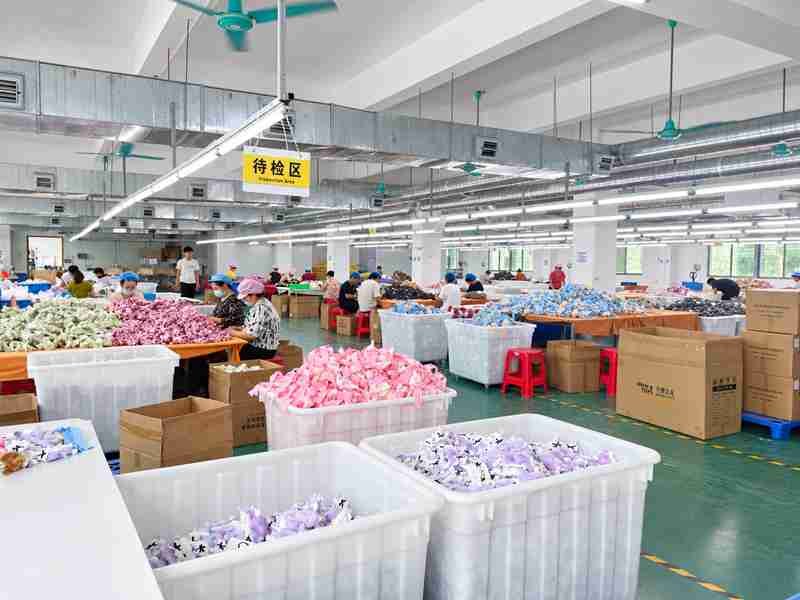
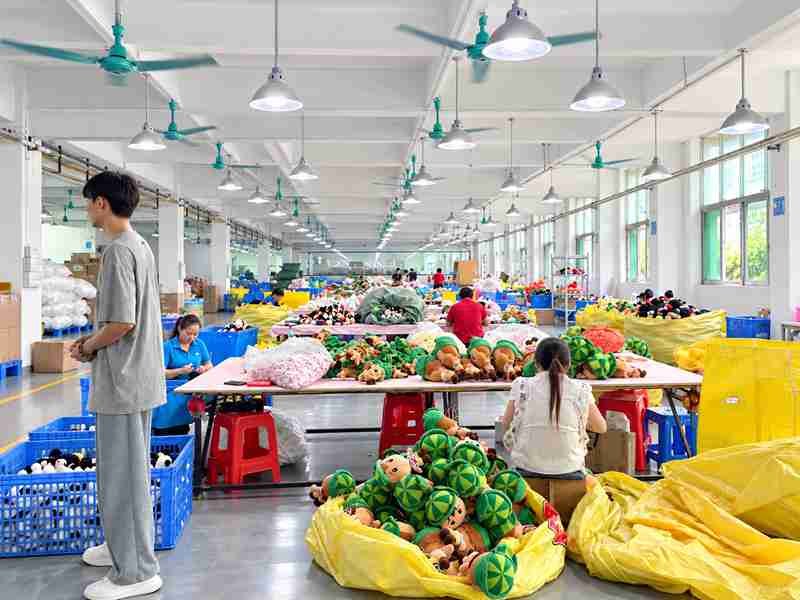
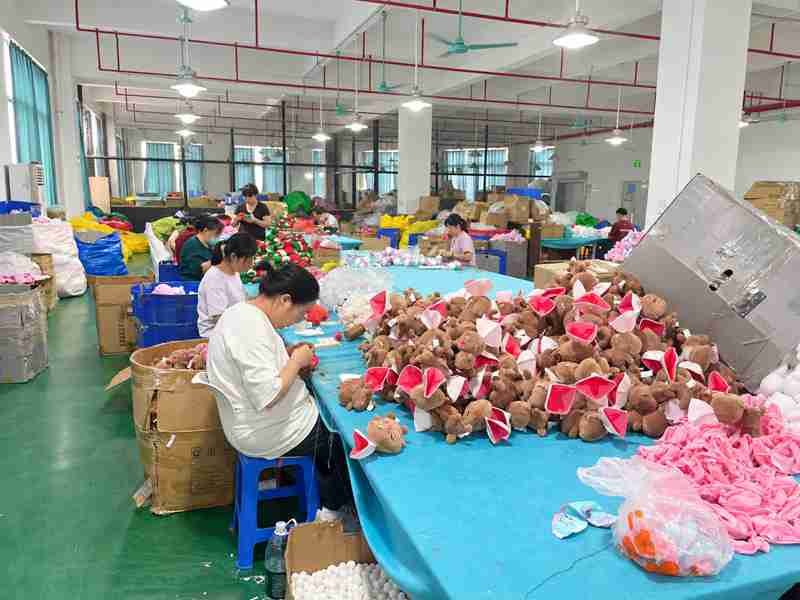
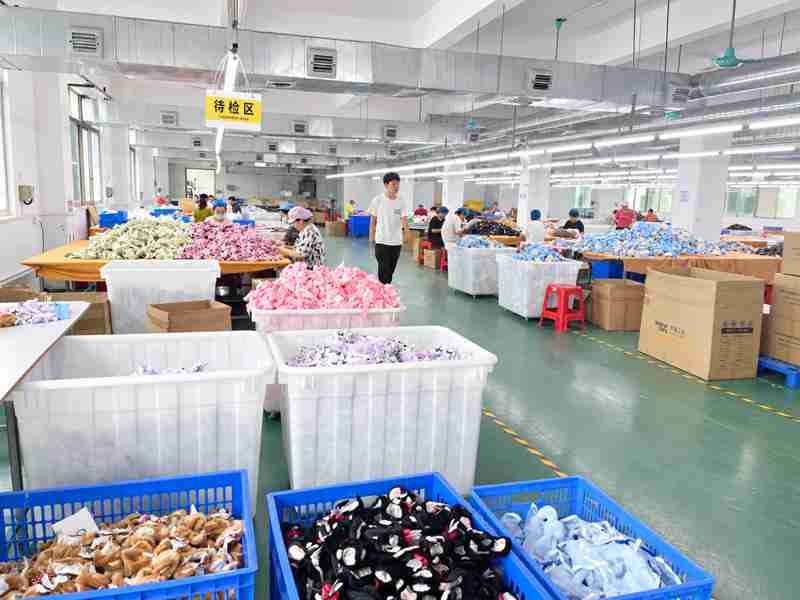
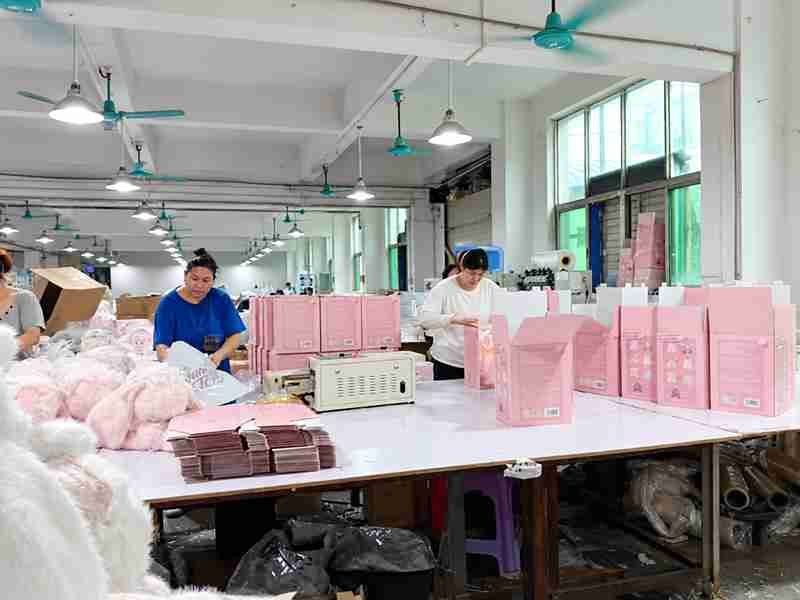
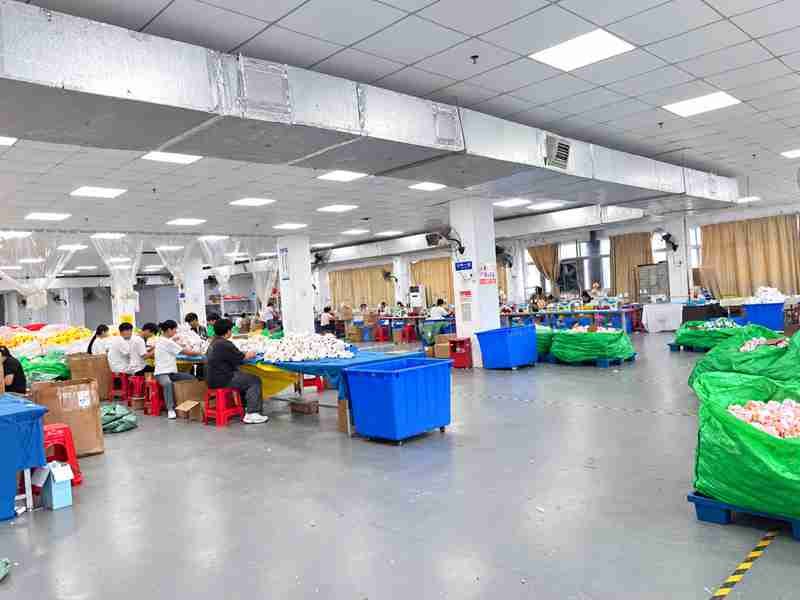
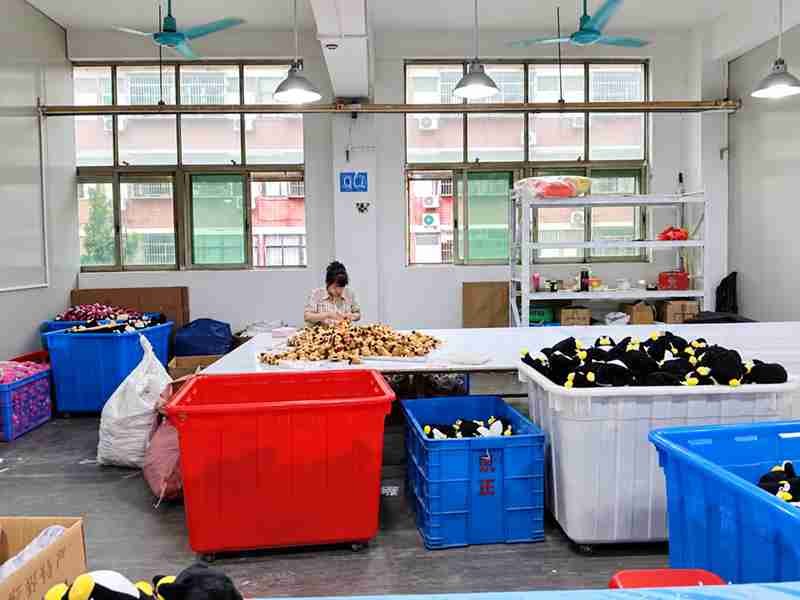
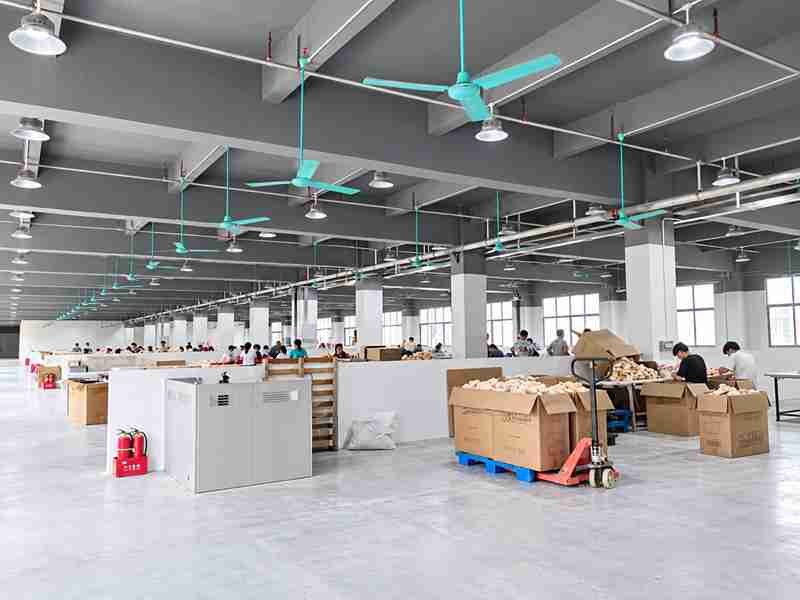
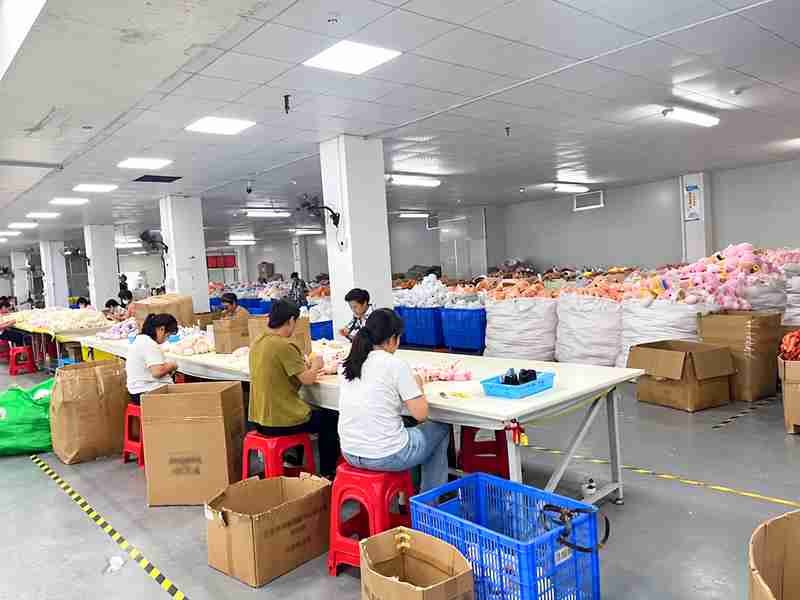
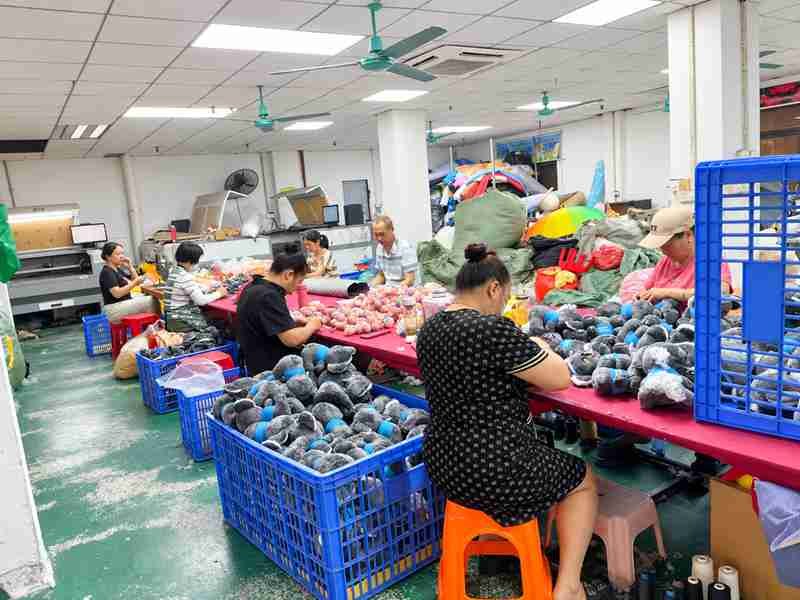
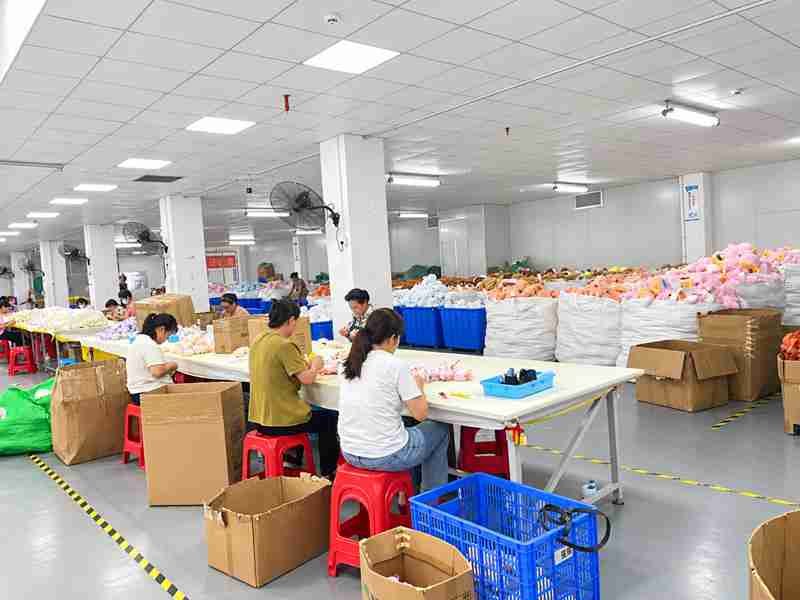
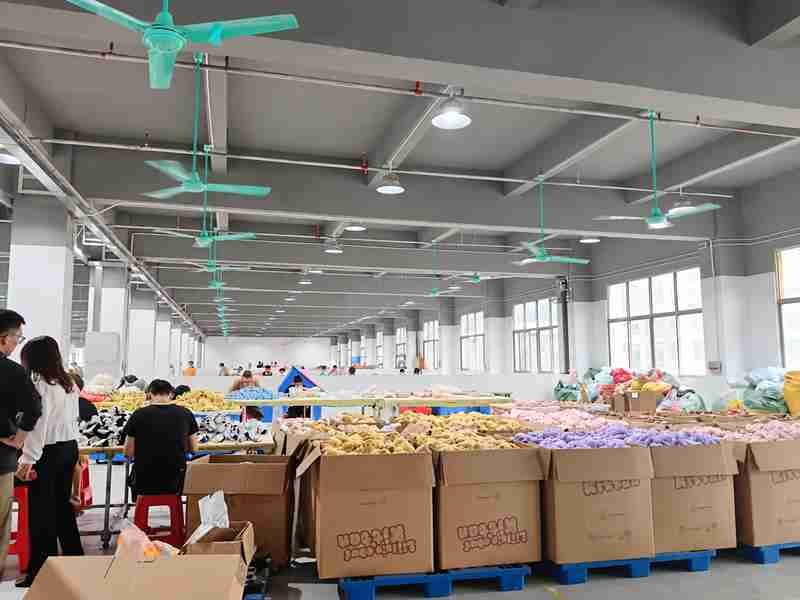
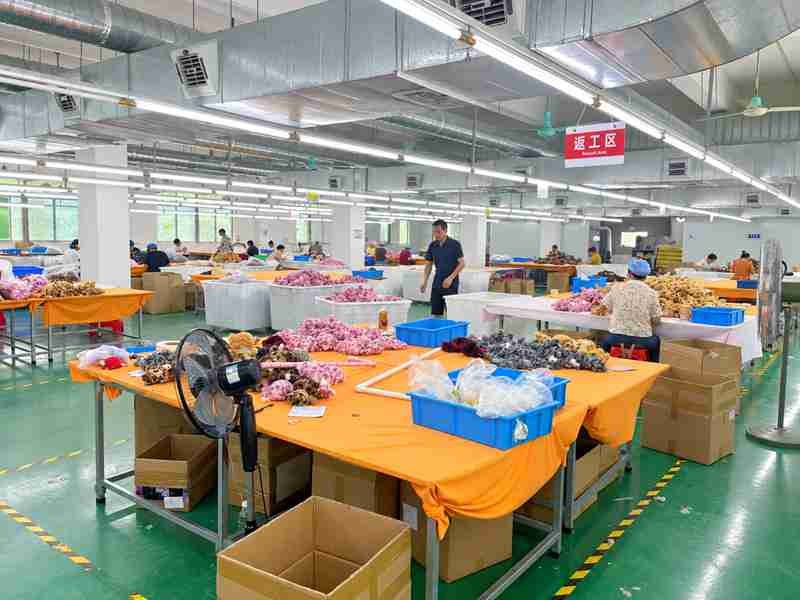
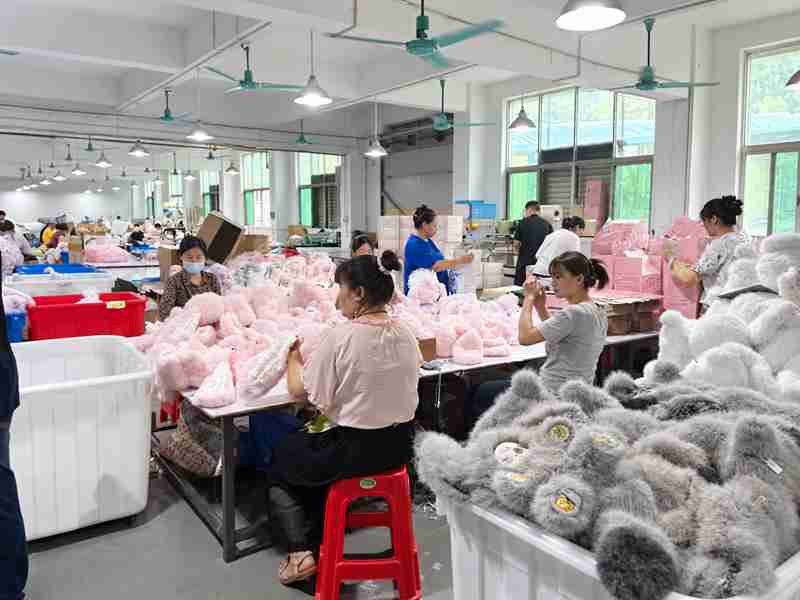
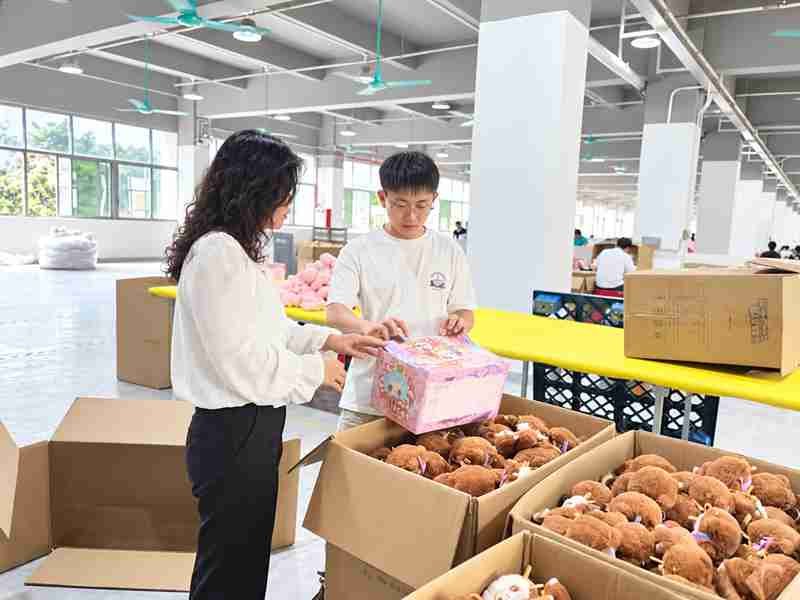
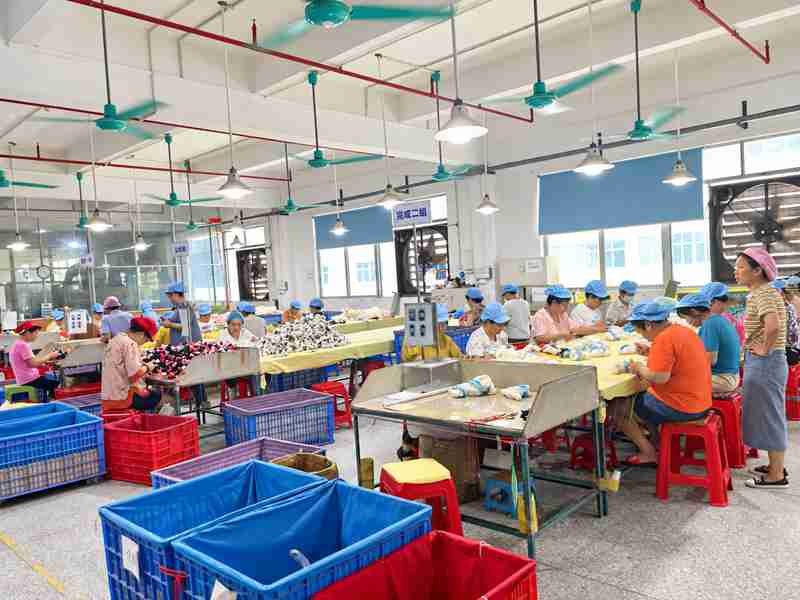
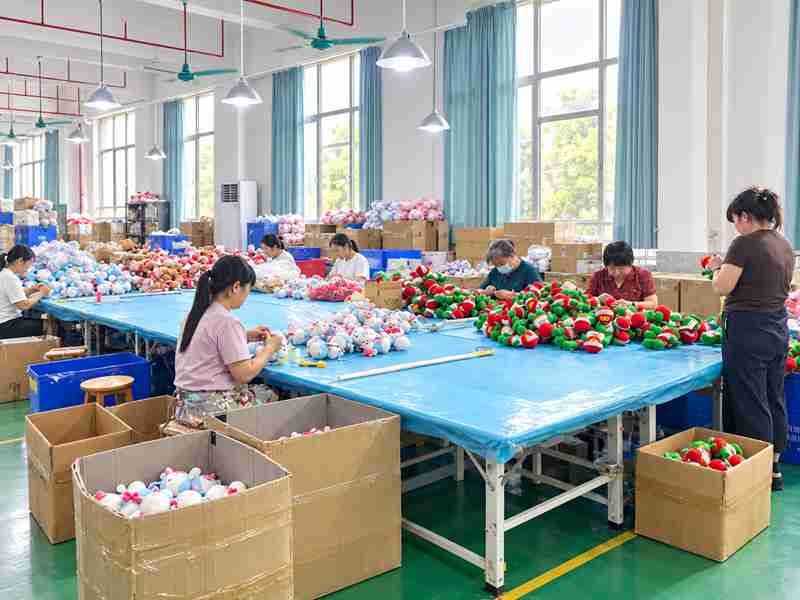
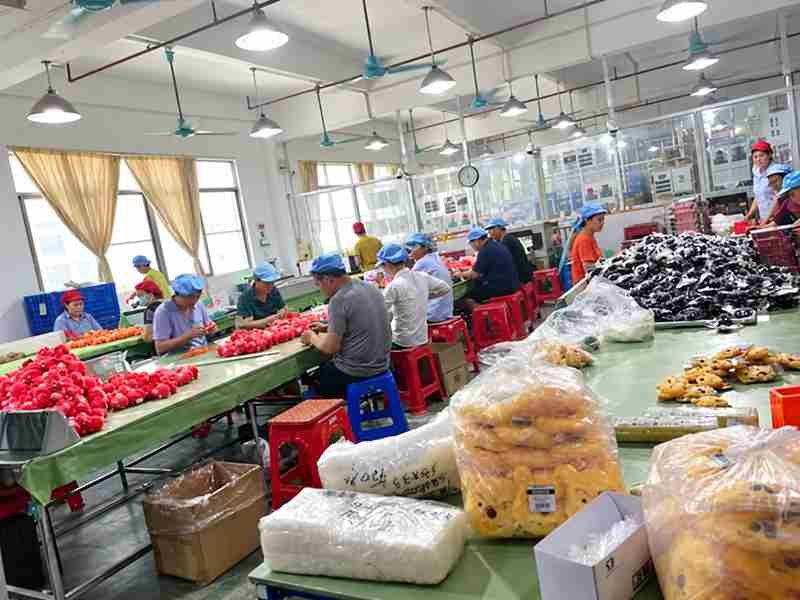
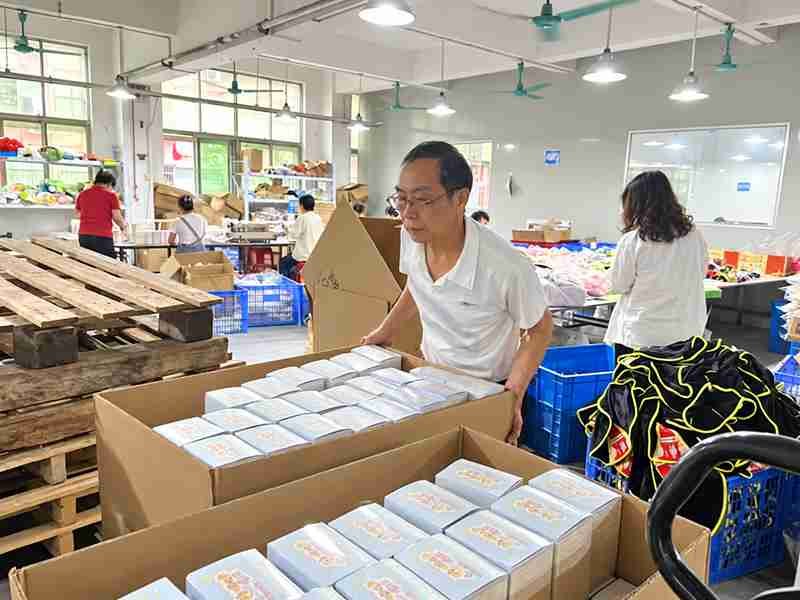
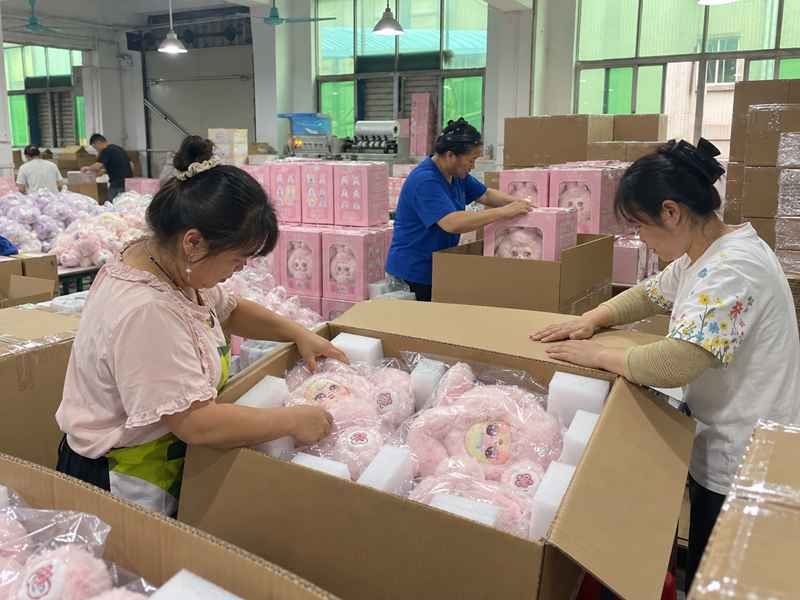
From Prototype to Production: Our Real Plush Factory Show
At Ewintoys, every plush project follows a structured development and production process, from initial design review and pattern making to sampling, mass production, quality inspection, and final delivery. Our real factory images provide a transparent view of how ideas are transformed into high-quality plush products through professional craftsmanship, engineering control, and careful production management.
Capacity Is Planned Around the Actual Product Mix
Factory scale becomes useful when production resources are matched to construction, SKU complexity, handwork, materials, and the required delivery window.
Product Complexity
SKU Mix
Pilot to Scale
Peak Season Planning
Quality Control Runs Through the Manufacturing Process
Quality gates are placed where problems can be prevented, contained, corrected, and traced rather than waiting for one final inspection.
IQC - Incoming Control
- Stops wrong materials before production.
- Keeps approved inputs tied to BOM and batch.
IPQC - Process Control
- Finds root process issues earlier.
- Prevents one defect from spreading through a large batch.
FQC - Finished Control
- Confirms the finished SKU before packing.
- Creates defect information for prevention and CAPA.
OQC - Outgoing Release
- Connects QC with packaging and shipment release.
- Reduces wrong-label, mixed-SKU, and pack-out errors.
Factory QC Lab Supports Physical and Process Verification
Internal test capability helps development and production find physical risks early, while formal regulatory testing remains project- and market-specific.
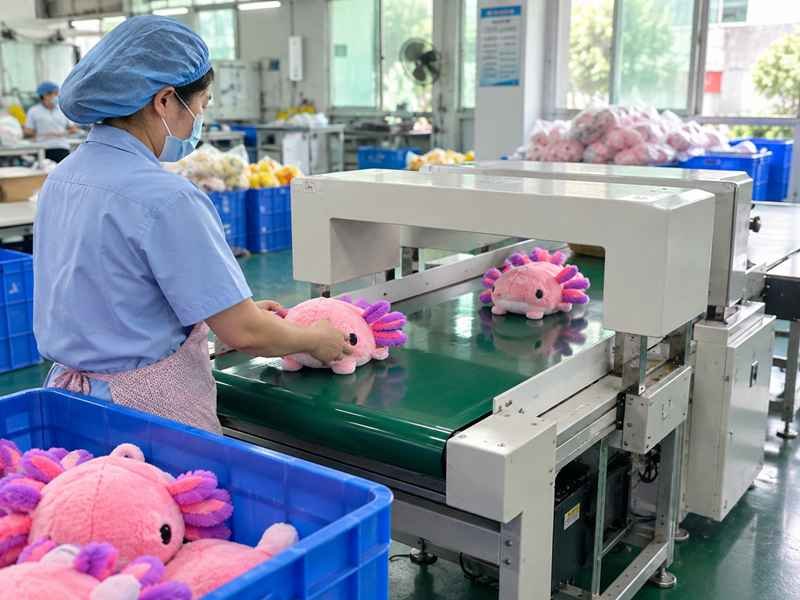
Needle & Metal Control
Needle and metal detection supports broken-needle and foreign-metal risk control after sewing and handwork. Equipment sensitivity, test pieces, calibration, product isolation, and broken-needle procedures matter more than simply passing finished goods through a detector once.
- Typical use: finished and post-handwork control.
- Factory role: detection, calibration, isolation, release support.
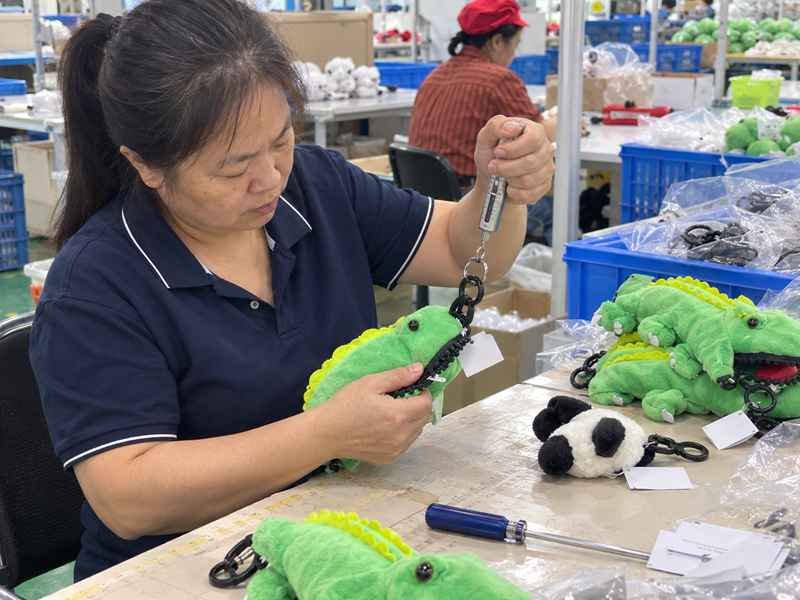
Pull & Torque
- Typical use: attached parts and hardware.
- Factory role: development pre-check and production verification.
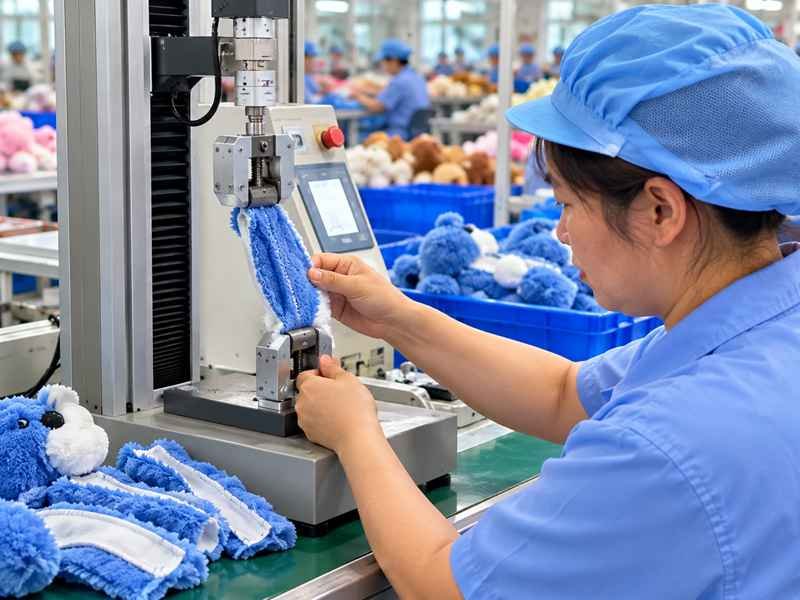
Seam & Tensile
- Typical use: seams and load-bearing structures.
- Factory role: process validation and defect diagnosis.
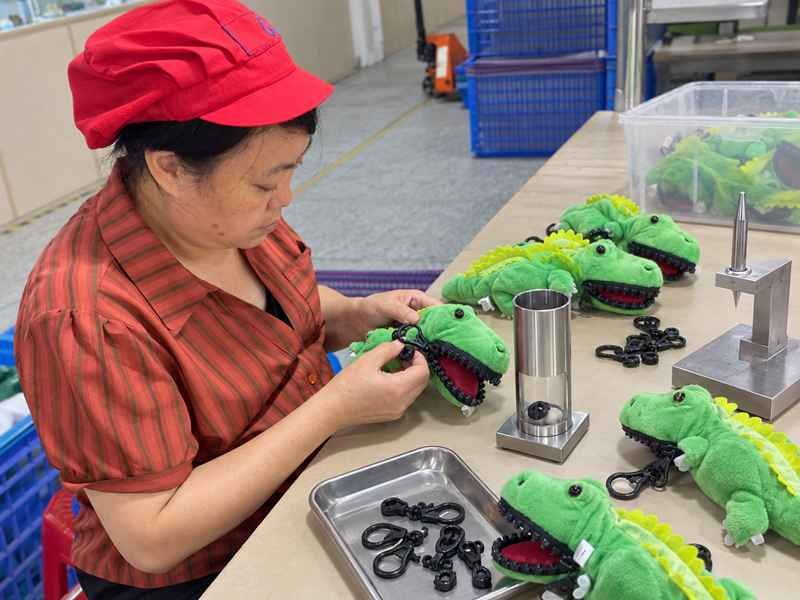
Small Parts & Sharp Points
- Typical use: hard components and detachable parts.
- Factory role: design and production pre-check.
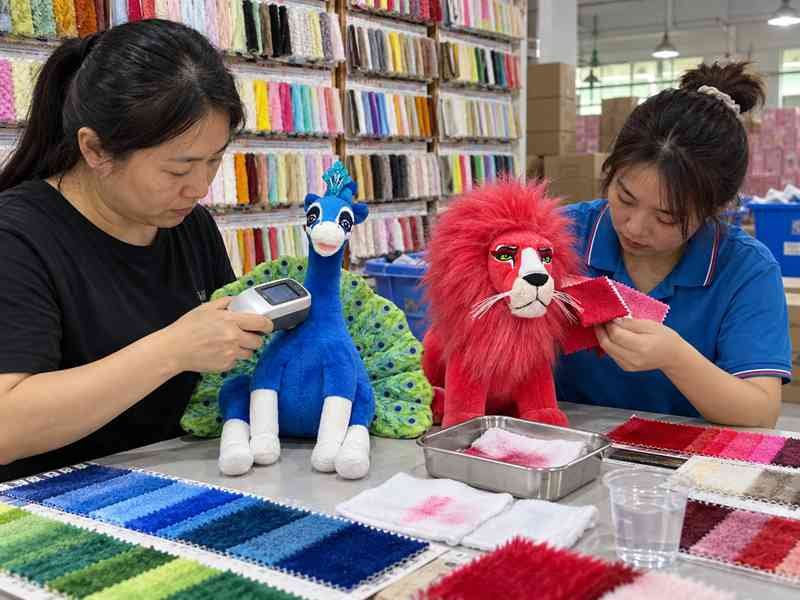
Color & Colorfastness
- Typical use: fabric, print, trim, and lot comparison.
- Factory role: incoming and development color control.
Drop & Compression
- Typical use: durability and packaging simulation.
- Factory role: development pre-check and process validation.
Defect Prevention Goes Beyond Final Inspection
Needle control, defect records, CAPA, and traceability help the factory prevent repeated problems and locate affected products when something goes wrong.
Needle Management
- Treat metal control as a process gate.
- Isolate affected product when an exception occurs.
Defect Records
- Connect each issue to the valid product version.
- Use recurring defects to improve prevention points.
CAPA
- Separate temporary containment from root correction.
- Verify effectiveness before closing systemic issues.
Traceability
- Link product and batch information across stages.
- Support targeted investigation instead of broad assumptions.
Certificates, Compliance & Quality Assurance
Ewintoys follows structured quality and compliance practices for custom plush production. We hold relevant certifications and support additional testing, inspection, and compliance documentation based on specific product requirements and destination markets, helping brands meet different international standards with confidence.
Packaging and Warehouse Control Finish the Factory Route
Qualified plush becomes a sellable and shippable unit only after packaging, labels, cartons, staging, and release data are correct.
Unit Packaging
Retail Packaging
E-Commerce Packaging
Master Cartons
Warehouse Staging
Shipment Release
Visit the Factory With a Clear Verification Plan
A factory tour is more useful when it follows the same route your project would take from development through production, quality, packing, and release.
Start in Product Development
Begin the visit where a custom plush actually starts: product development. Review how artwork, reference products, patterns, materials, sample versions, Golden Samples, and project files are organized before a new SKU reaches bulk production.
For an active project, send artwork, an existing sample, a SKU list, or the current supplier problem before the visit. The team can then show how Ewin would approach the specific development and manufacturing questions instead of giving only a generic showroom tour.
Useful verification points include pattern and sample identification, material approval, revision records, development handoff, and how a final sample becomes production information. Confidential client projects remain subject to restricted access and photography controls.
Walk the Production Route
Follow the actual manufacturing sequence through material handling, cutting, embroidery or printing, sewing, stuffing, hand assembly, finishing, and production control. Look for how product identity, pattern revision, material, bundles, workstations, and in-process checks remain connected as the plush moves between departments.
A meaningful factory visit should show more than busy machines. Ask how long-pile fabric direction is controlled, how similar SKUs are kept separate, how first pieces are approved, how filling is standardized, and how accessories or modules are installed consistently.
For larger programs, the visit can also discuss how product complexity, SKU mix, handwork load, forecast, and delivery window affect capacity planning rather than relying on one generic output number.
Review QC, Packaging and Warehouse
Continue through internal QC and physical-test areas, then follow approved products into packaging, master-carton preparation, warehouse staging, and shipment release. This verifies that Ewin’s responsibility does not stop after sewing and that the commercial unit is controlled through the final factory handoff.
Useful QC discussion points include IQC/IPQC/FQC/OQC, needle management, pull or seam checks, defect records, CAPA, traceability, and the boundary between internal pre-checks and third-party regulatory testing.
In packaging and warehouse areas, review label or barcode control, carton configuration, SKU separation, destination staging, and final release data. Those steps are especially important for retail, Amazon, multi-SKU, and multi-destination programs.
Choose On-Site or Video Tour
Ewin can use an on-site visit for sourcing, quality, product, licensing, or supply-chain teams that need direct factory verification. When travel is not practical, a live video factory tour can follow a pre-agreed route and focus on the operations most relevant to the proposed project.
Before scheduling, share the company name, role, product category, main verification questions, preferred date, and whether an active project should be discussed. That lets the visit include the right development, manufacturing, quality, or project personnel where appropriate.
Factory tours do not override confidentiality controls. Unreleased client products, restricted documents, photography-limited areas, or sensitive production information may be excluded or shown only in a controlled form to protect existing projects.
Frequently Asked Questions
Yes. Ewin Toys operates an integrated plush development and manufacturing system covering development, material handling, cutting, decoration, sewing, stuffing, assembly, QC, packaging, warehousing, and shipment preparation.
Ewin manufactures core custom plush, character and mascot plush, collectibles, mini and blind-box plush, keychains, hybrid products, electronic or AI-enabled plush, and lifestyle merchandise using soft-goods construction.
Yes. A factory visit can be arranged for qualified commercial projects. Share your company, role, project type, main verification questions, and preferred timing so the visit can follow a useful manufacturing route.
Yes. A live video tour can focus on development, materials, production, QC, packaging, or other relevant areas. Confidential projects and restricted client information remain protected during any tour.
Approved fabric should be tied to material identity, composition, GSM, pile or thickness, color, nap, supplier route, and sample approval. Incoming checks then verify applicable points before material is issued.
Accessories can be defined by part ID, material, size, color, weight, quantity, position, fixing method, and installation notes, with relevant strength, function, appearance, or safety checks added by project.
Bulk production is released from the approved Golden Sample together with the frozen BOM, released pattern, current artwork, measurements, accessories, QC requirements, and packaging revision – not from an informal sample.
Ewin uses staged IQC, IPQC, FQC, and outgoing release controls supported by product references, physical or process checks, defect records, CAPA, needle control, and traceability where applicable.
Yes. Program planning can connect SKU identity, sample version, BOM, materials, packaging, barcode, production wave, QC status, shipment, and forecast so many products remain distinguishable during execution.
Send your company information, product type, artwork or sample, approximate size, SKU count, quantity, market, launch timing, current supplier concerns, and the areas you want to verify during the visit.
Book a Factory Tour or Manufacturing Review
Tell Ewin what you want to verify before the visit so the factory tour can focus on the manufacturing decisions that matter to your project. Share your company, business email, product type, artwork or physical sample, approximate size, SKU count, quantity, target market, launch timing, and current project stage. If you already work with another supplier, explain the manufacturing, quality, capacity, communication, or delivery issue you want Ewin to review. Choose an on-site visit or live video factory tour and provide a preferred date when available. You can also upload a SKU list, specification, existing sample photos, retailer requirements, or QC checklist so the appropriate development, manufacturing, quality, or project personnel can prepare for the discussion.
Suggested information:
- Company
- Business Email
- Company Website
- Customer Type
- Product Type
- Artwork / Sample Available
- Approx. Product Size
- SKU Count
- Estimated Quantity
- Target Market
- Target Launch Date
- Main Verification Requirement